CNC Cost vs Lead Time: Impact of CMM Inspection Frequency
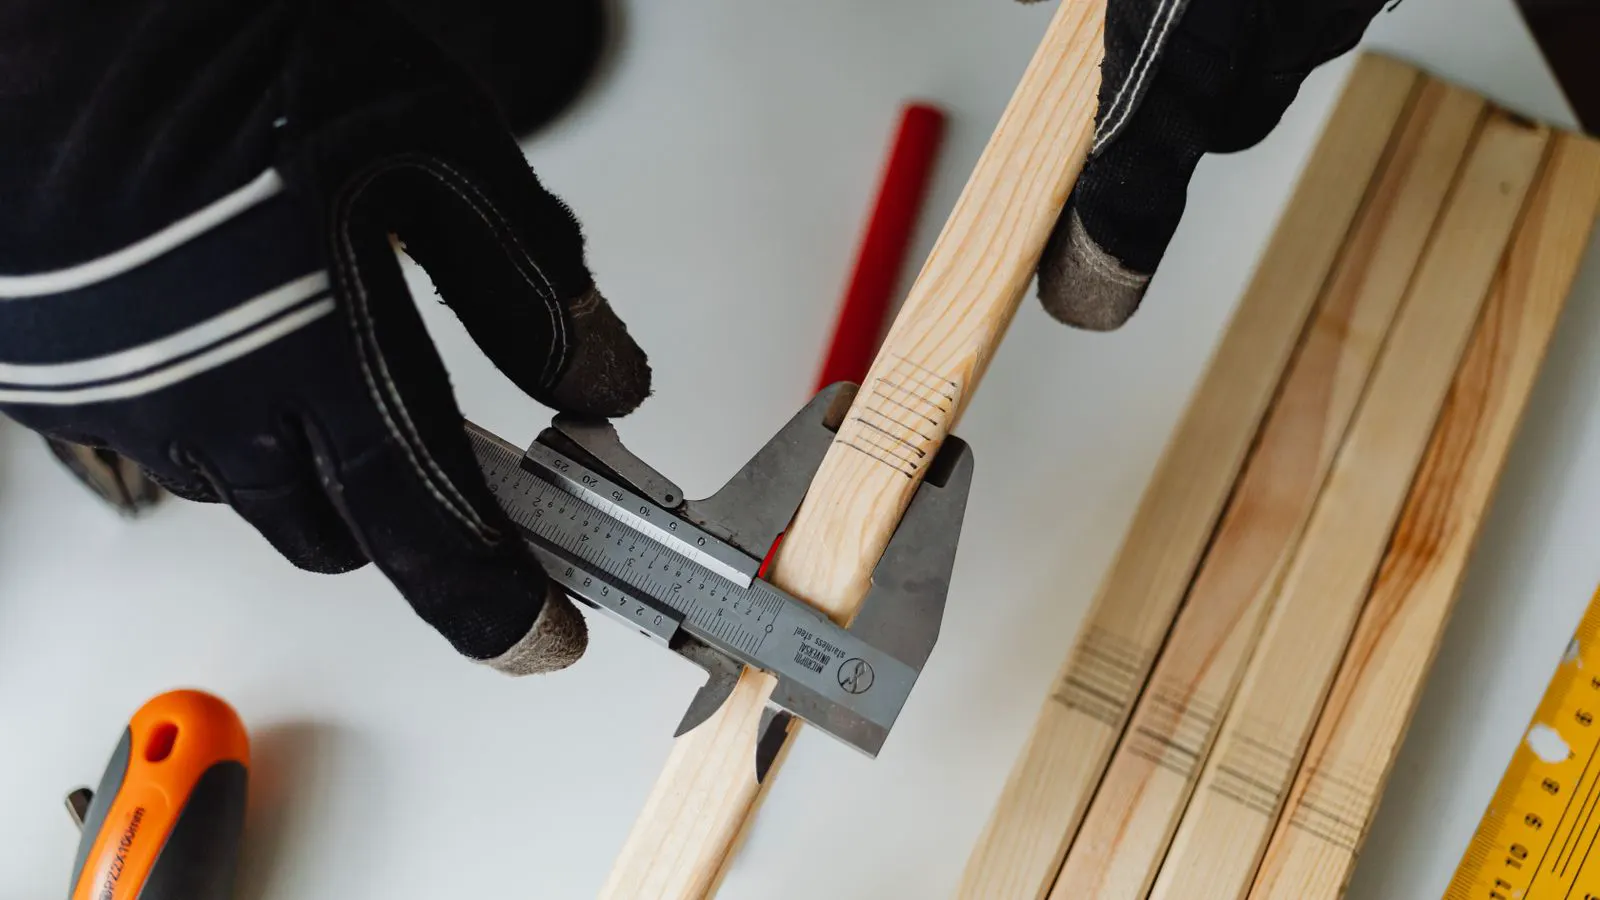
More frequent cmm inspection improves cnc quality control but adds time and expense. This guide explains how to set inspection intervals, analyze costs, and write RFQs that match your tolerance and delivery needs.
- More frequent cmm inspection raises cnc quality control reliability but extends lead time and adds measurement cost.
- Match inspection frequency to part criticality, tolerance class, and material, not to a blanket rule.
- Use a quality cost analysis to compare rework, scrap, and inspection expense against the value of the part.
- Write clear RFQs that state inspection frequency, acceptance criteria, and reporting requirements so quotes compare fairly.
- CMM data supports traceability and supplier audits, but over-testing can slow production without improving fit.
What sets the inspection frequency?
Inspection frequency starts with part criticality. A aerospace bracket with tight tolerance windows needs tighter control than a standard machine housing. The first decision is where the part sits in the assembly. If a surface must mate with a bearing, seal, or sensor housing, the cnc quality control plan must protect that feature. If the feature only requires general fit, inspection can be less aggressive.
Material affects the decision too. Aluminum responds quickly to tooling wear and thermal drift. Stainless and titanium hold geometry longer but often require more attention at the start of the run. Castings and forgings add variability that raw bar stock does not. The material behavior determines how often the shop should check the first piece, the mid-run piece, and the final piece.
The tolerance class drives the frequency more than anything else. A plus or minus 0.05 mm tolerance allows more measurement spacing than a plus or minus 0.005 mm tolerance. When the tolerance window is small, the cost of a single missed defect can outweigh the cost of measuring every piece. The inspection frequency is a balance between measurement effort and the financial risk of a bad part reaching the customer.
How does cmm inspection change lead time?
Every cmm inspection adds time to the production sequence. The part must move from the machining cell to the metrology lab. It must be clamped or supported without changing its reference. The operator must load the program, run the measurement, and record the data. Then the part returns to the next process.
The added time depends on the number of features checked. A simple block with three critical dimensions may take minutes. A complex aerospace bracket with multiple datums, thread features, and surface checks can take longer. The cmm program itself also matters. A well-built program runs faster than a poorly organized one.
Lead time also depends on where the check happens. A first article check happens before the run starts. A mid-run check happens after a defined number of parts. A final check happens before shipment. Each stage creates a decision point. If the check fails, the shop must stop, rework, and recheck. That rework loop can add hours or days depending on the complexity of the fix.
How to write a clear RFQ for cnc quality control
A clear RFQ removes guesswork. State the inspection frequency directly. For example, require first article, mid-run, and final inspection. State the acceptance criteria. Use the drawing tolerances, not vague language such as as close as possible. State the measurement method. If the part needs CMM data, say so. If the part needs a functional gauge, say that instead.
The RFQ should define what data the supplier provides. A certificate of conformance is a statement that the part meets the drawing. CMM data is a measurement record. Some buyers need the raw data. Some need a summary report. Others need a full report with graphs. The more data you request, the more the supplier must spend on measurement and documentation.
The RFQ should also state what happens on a failure. Does the supplier scrap the part? Does it rework the part? Does it hold the lot? A clear failure protocol prevents disputes. It also helps the supplier plan the process. If the buyer expects the supplier to hold the entire lot for recheck, the supplier must reserve space and time for that event.
Cost drivers in a quality cost analysis
A quality cost analysis compares the cost of inspection with the cost of defects. The inspection side includes machine time, operator time, program development, calibration, and reporting. The defect side includes rework, scrap, expedited shipping, customer downtime, and warranty claims.
The table below shows the main cost drivers in a typical cnc quality control plan. The values are general. Actual cost depends on part size, complexity, material, and supplier rates.
| Cost Driver | What It Affects | Typical Impact |
|---|---|---|
| Inspection frequency | Metrology time and labor | Higher frequency raises cost and extends lead time |
| Feature count | CMM program length | More features increase measurement time |
| Part size | Fixture setup and access | Larger parts take longer to position and measure |
| Tolerance class | Measurement method and operator skill | Tighter tolerances need more attention and sometimes different equipment |
| Material | Machine setup and tooling | Exotic materials add setup time and may need special fixtures |
| Reporting format | Documentation effort | Raw data and graphs cost more than a simple certificate |
The cost of inspection is not only the CMM charge. It is also the cost of the part sitting in the metrology queue. If the shop has one CMM and five machining cells, the metrology lab becomes a bottleneck. The part waits for the machine. The waiting time is not always visible on the quote, but it is part of the lead time.
How to compare quotes fairly
Two quotes can look similar on price but differ greatly in inspection practice. One supplier may include first article and final inspection. Another may charge extra for CMM data. A third may only provide a certificate of conformance without measurement records. The buyer must ask for the same level of documentation before comparing prices.
Compare the lead time breakdown. Ask how many days the supplier reserves for inspection. Ask whether the CMM check is included in the quoted lead time or added on top. Ask what the supplier does when a part fails. If the supplier holds the lot for recheck, the lead time increases. If the supplier scrappes the part and runs a new piece, the lead time increases.
Also compare the measurement method. A CMM check is precise, but it is slow. A functional gauge can be faster, but it may not capture every feature. A vision system can check surface features, but it may not measure depth or thread form. The method must match the feature being controlled. A quote that uses the wrong method may save money now and create a problem later.
When to increase inspection frequency
Increase inspection frequency when the part has a history of failure. A supplier audit may show that a certain feature drifts after a certain number of parts. A material change can introduce new variability. A new tooling setup can change the cutting dynamics. Each of these factors is a reason to check more often.
Increase inspection frequency when the part is new. A first production run has more uncertainty than a mature run. The supplier has not yet learned the exact behavior of the process. The first few pieces carry more risk. After the process stabilizes, the frequency can move to a standard interval.
Increase inspection frequency when the buyer sees a pattern in returned parts. If the same feature fails repeatedly, the root cause is not fixed. More inspection will catch the bad part, but it will not fix the process. The buyer should ask the supplier to perform a root cause analysis and provide corrective action. Then the inspection plan can be adjusted to match the new process capability.
How to balance cost, quality, and delivery
The balance point is where the cost of inspection equals the expected cost of defects. If the part is cheap and the tolerance is loose, inspecting every piece may cost more than the part is worth. If the part is expensive and the tolerance is tight, inspecting every piece may be justified. The buyer must know the value of the part and the cost of a failed part.
The buyer also must know the delivery window. A strict delivery date may require a faster inspection method. A flexible delivery date may allow a full CMM check on every piece. The RFQ should reflect this trade-off. If the buyer needs the part in five days, the inspection plan must fit that window. If the buyer can wait two weeks, the shop can use a slower, more thorough method.
The final decision is a business decision, not just a technical one. The buyer should weigh the risk of a bad part against the cost of extra measurement. The supplier should weigh the cost of inspection against the risk of a customer complaint. Both sides should agree on the inspection plan before the first piece is cut.
Frequently asked questions
How often should a CMM inspect a CNC part?
There is no single answer. The frequency depends on tolerance, material, part criticality, and supplier capability. A common plan uses first article, mid-run, and final checks.
Does cnc quality control always require CMM inspection?
No. Some parts can use functional gauges, vision systems, or direct measurements. CMM is best for complex geometry and tight tolerances.
How does inspection frequency affect lead time?
More checks add metrology time, queue time, and decision time. A failed check adds rework and recheck time, which can extend delivery.
What should I put in the RFQ for cnc quality control?
State the inspection frequency, acceptance criteria, measurement method, reporting format, and failure protocol. This makes quotes comparable.
How can I reduce quality cost without lowering quality?
Match the inspection method to the feature being controlled. Use CMM for tight geometry and functional gauges for simple dimensions. Fix process problems so fewer checks are needed.