Steel vs Aluminum: CNC Tolerance and Surface Finish
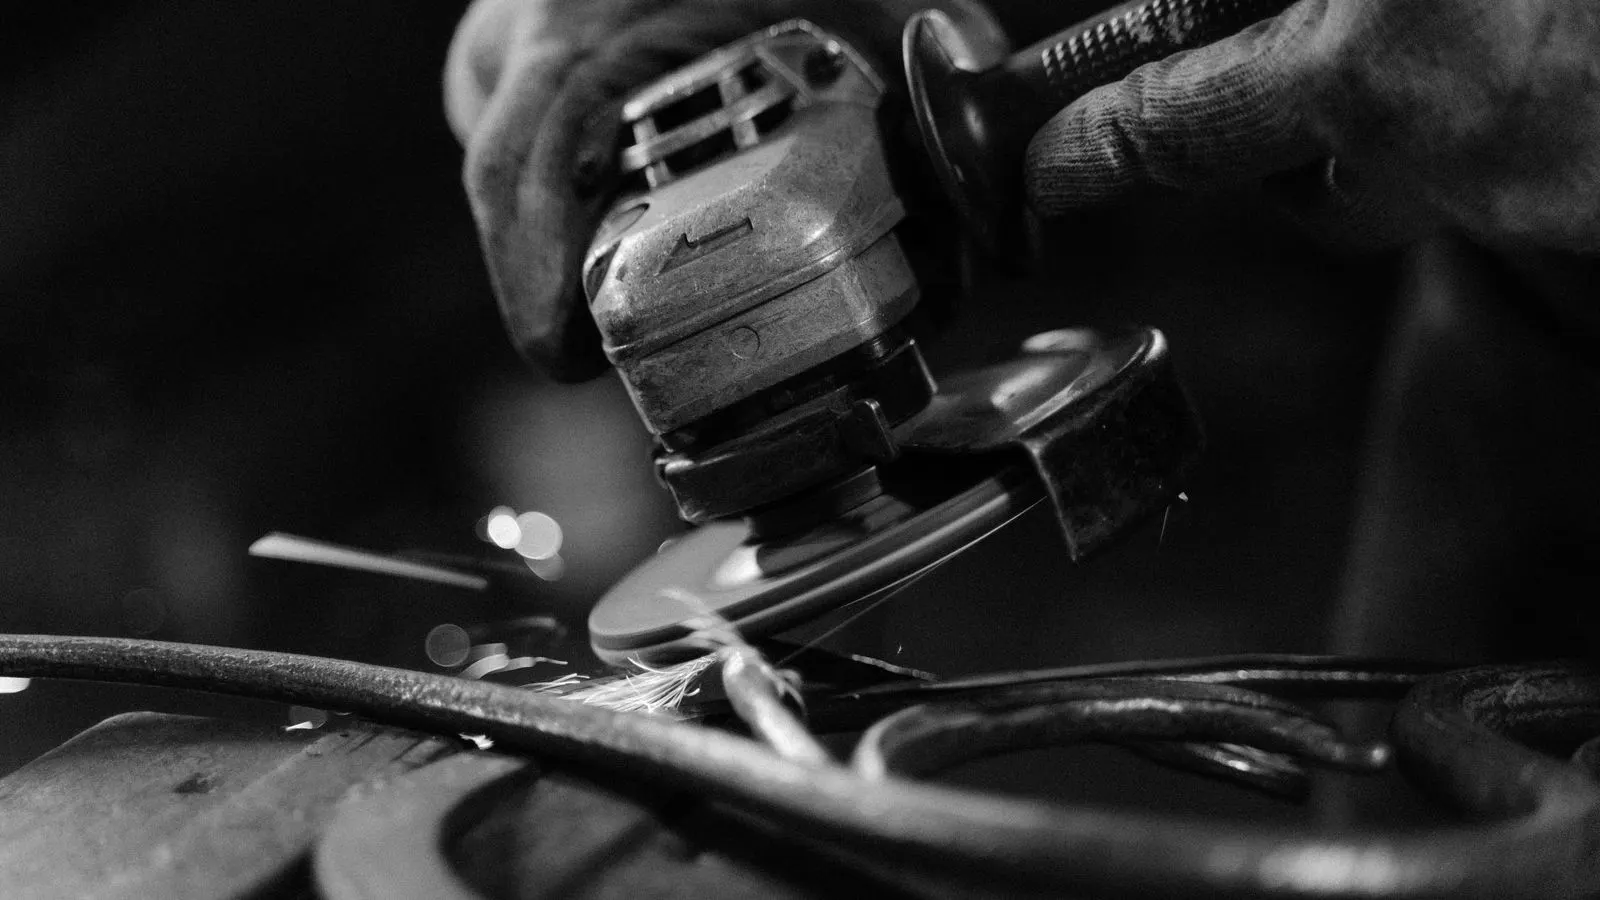
Steel offers tighter dimensional stability but often needs post machining for a fine finish. Aluminum holds tolerances well after heat but is softer, requiring careful tooling for smooth surfaces. The right choice depends on part function, batch size, and cost.
- Steel is harder and less springy, so it holds tight tolerances better under load, but it is tougher to machine and often leaves a rougher finish if the tooling is not right.
- Aluminum cuts fast and holds fine detail, but it is soft and can smear or stick, so surface finish depends heavily on chip control and tool speed.
- For tight dimensional work, steel usually wins. For lightweight parts and visible surfaces, aluminum can be the better choice if the finish is managed properly.
- The gap between the two materials narrows when you control coolant, tool geometry, and post processing steps like polishing or anodizing.
How Steel and Aluminum Behave in the Machine
Steel and aluminum do not behave the same way under a cutting tool. Steel is harder, denser, and less likely to spring back when the load changes. Aluminum is softer, lighter, and more likely to smear, stretch, or stick to the tool if the cut is not set up correctly. These differences show up in two places that matter most: dimensional accuracy and surface finish.
A machinist who has run both materials will tell you the same thing. Steel is more forgiving when it comes to holding size. If a part has a critical hole or a flat face, the material itself works in your favor. It does not deform as easily during the cut, and it does not spring back as much when the tool is withdrawn. Aluminum is different. It is easy to cut, but it is also easy to push around. A soft chip can wrap around the tool. The workpiece can flex on the vise. The finish can look great on the first pass and then change once the part is unloaded.
The result is not that one metal is better than the other. It is that each one has a different failure mode. Steel usually fails in finish quality if the tool is dull or the speed is wrong. Aluminum usually fails in dimensional consistency if the fixturing is loose or the chip control is poor. Understanding where each material breaks tells you what to control.
Tolerance Control: Where Steel Holds Its Ground
When you are chasing a tight tolerance, steel has a structural advantage. It is stiffer. That means the part does not move as much when the cutting forces change. For a machinist, this makes repeatable cuts easier. If you cut a bore to a specific size, then load the part, the size is less likely to drift. Aluminum is more prone to that kind of movement, especially in thin walls or long unsupported features.
This does not mean aluminum cannot hit tight tolerances. It can. But the process has to be managed differently. You need stable tooling, consistent feed rates, and a setup that does not let the part shift. A soft aluminum part in a vise can flex just enough to change the size of a slot by a few thousandths of an inch. That is often within spec, but it is not the same as the predictability you get from steel.
For parts that go into assemblies where clearance or interference is critical, steel is the safer default. If the part is a bearing race, a guide bushing, or a precision interface, the stiffness of steel makes the tolerance easier to defend. Aluminum works well for housings, brackets, and light structural parts where the tolerance is a bit looser and the finish is more important than absolute stiffness.
Surface Finish: The Soft Material Problem
Surface finish is where the comparison gets interesting. A finished aluminum part can look like a mirror. A finished steel part can look like brushed metal. But getting there is not just about the material. It is about how you cut it.
Aluminum is soft, which sounds like it should make a smooth cut. In practice, softness creates a problem called built up edge. The aluminum can smear onto the tool instead of breaking away cleanly. The result is a dull, fuzzy surface, even if the part is within tolerance. Steel does not smear the same way. It chips. That means the surface is usually cleaner, but the tool has to be sharp and the speed has to be right. A dull tool on steel leaves a scratchy, torn finish. A dull tool on aluminum leaves a smeared, shiny one.
The trick with aluminum is to keep the chip flowing. This means the right tool geometry, the right speed, and usually some form of air or coolant to push the chip away. If the chip stays on the tool, the finish degrades quickly. Steel is more forgiving in that sense, but it is less forgiving in another way. If the tool is not sharp, the surface finish on steel is visibly rougher than it would be on aluminum with a sharp tool.
When to Pick Each Material for Dimensional Work
The choice between steel and aluminum for tolerance work comes down to part function and production reality. Here is how the trade-offs break down in practice.
| Option | Best for | Limitations |
|---|---|---|
| Carbon steel | Tight tolerances, high strength, load bearing parts | Rougher finish without post work, longer cycle times, higher tool wear |
| Alloy steel | Precision parts, hardened surfaces, wear resistance | Higher cost, harder to machine, needs heat treatment planning |
| 6061 aluminum | Lightweight parts, general machine parts, visible surfaces | Softer, can smear, needs careful fixturing for tight tolerances |
| 7075 aluminum | High strength to weight, aerospace and automotive parts | More expensive, harder to machine than 6061, still softer than steel |
| Stainless steel | Corrosion resistance, medical and food parts | Very hard to machine, high tool wear, long cycle times |
Carbon steel is the workhorse for parts that need to hold a size under stress. It is cheap, predictable, and stiff. The trade-off is finish. If the part will be seen, you may need a polishing step, a bead blast, or a coating to make the surface acceptable. That adds cost and lead time.
Aluminum is the choice when weight and finish matter more than absolute stiffness. 6061 is the most common alloy for general CNC work. It machines well and takes an anodize well, which gives you a durable finish that also hides minor machining marks. 7075 is stronger, but it is more expensive and a bit harder to cut. It is used when the part needs to be light but still strong enough for structural loads.
Stainless steel sits in a middle ground that is often misunderstood. It is a steel, so it is stiff. But it is also tougher to machine than carbon steel. The finish can be good, but the cycle time is longer and the tool wear is higher. For tight tolerances, stainless is a good choice, but you should budget for the extra machining time.
When to Pick Each Material for Visible Surfaces
If the part will be seen, the finish story changes. Aluminum is easier to get to a high gloss finish because it is soft and takes a polish well. Steel is harder to polish, but it can be brushed, bead blasted, or coated in ways that give it a different look. The best choice depends on the aesthetic you want.
A visible aluminum part can be anodized to a flat, matte finish that hides minor scratches and machining marks. That is why aluminum is so common for consumer electronics, camera housings, and light enclosures. The anodize layer is hard, it is colored, and it protects the soft metal underneath. The surface finish after anodizing is consistent and predictable.
Steel is often chosen for visible parts when the look is industrial. Brushed stainless, black oxide, or a powder coat gives the part a rugged appearance. The surface does not need to be mirror smooth. It needs to be consistent. For that kind of finish, the material choice is less about the metal and more about the post processing. A steel part can look better than an aluminum part if the finish process is right, and vice versa.
How Post Processing Changes the Comparison
The raw machined finish is only part of the story. Post processing can close the gap between steel and aluminum. Polishing, bead blasting, anodizing, painting, and plating all change how the part looks and feels.
For aluminum, anodizing is the go-to finish. It gives you color, hardness, and a matte surface that hides minor marks. If you need a mirror finish, you can polish the aluminum before anodizing. That is a lot of work, but it is possible. For steel, polishing is harder because the metal is harder. You may need multiple grits and a lot of time. Bead blasting is a good middle ground. It gives you a uniform matte finish without the cost of polishing.
The key is to decide on the finish before you choose the material. If the finish is a flat black anodize, aluminum is probably the better choice. If the finish is a brushed stainless look, steel is the obvious choice. If the finish is a powder coat, either metal works, but the surface prep will be different. Aluminum needs cleaning and priming. Steel needs rust prevention and a different primer.
Practical Checks Before You Commit
Before you pick a material, run a few practical checks. First, look at the tolerance. If the part has a critical feature that must hold size under load, steel is the safer bet. If the tolerance is looser and the part is lightweight, aluminum is a strong option. Second, look at the finish. If the part is visible and needs a matte color, aluminum with anodizing is a good fit. If the part is industrial and needs a brushed look, steel is easier.
Third, look at the batch size. Aluminum machines faster, so for small batches where cycle time matters, it can be cheaper. Steel machines slower, but it is often cheaper per kilogram. For large runs, the material cost and cycle time both matter. For small runs, the setup cost and the finish quality are the bigger factors.
Fourth, look at the tooling. Aluminum is soft, so you need sharp tools to avoid built up edge. Steel is hard, so you need tough tools to avoid chipping. If your supplier has good tooling for the material you choose, the difference in finish narrows. If they are not set up for that material, the finish will suffer no matter what you pick.
Final Word on Material Selection
Steel and aluminum are both common in CNC machining, but they do not give you the same result. Steel gives you stiffness and predictable tolerances. Aluminum gives you lightness and a finish that is easy to make attractive. The right choice is not about which metal is better. It is about which metal fits the part function, the finish requirement, and the production reality.
If the part needs to hold a size under stress, pick steel. If the part needs to be light and look good, pick aluminum. If the part is in between, look at the post processing. A well finished aluminum part can beat a rough steel part. A well finished steel part can beat a smeared aluminum part. The material is the starting point. The process is what decides the outcome.
Frequently asked questions
Can aluminum hold tighter tolerances than steel?
Yes, but it requires careful fixturing and consistent cutting speeds. Aluminum is softer and more prone to spring back, so the setup has to be more stable to keep the size repeatable.
Which material is easier to get a smooth finish on?
Aluminum is easier to polish to a high gloss because it is soft. Steel is easier to get a consistent brushed or matte finish. The raw machined finish on aluminum is more prone to smearing if the tooling is not right.
Is steel more expensive than aluminum for CNC parts?
It depends on the alloy and the finish. Carbon steel is often cheaper per kilogram than aluminum, but the cycle time is longer. 7075 aluminum can be more expensive than 6061, and stainless steel is often the most expensive of the three.
Does stainless steel machine like carbon steel?
No. Stainless steel is tougher and gummier. It wears tools faster and produces longer chips. The cycle time is higher, and the finish can be rougher if the tooling is not sharp.
Should I choose aluminum for a part that will be painted?
Yes, aluminum is a good choice for painted parts because it is light and takes a primer well. Steel also works, but it needs rust prevention and a different prep. The paint finish will hide minor machining marks on both materials.