Fixing Chatter Marks on CNC Machined Aluminum Parts
Chatter marks on aluminum CNC parts result from vibration during cutting. Fix them by adjusting cutting parameters, improving tool rigidity, and verifying workholding stability. These adjustments reduce the defect and improve surface finish for final assembly.
- Reduce spindle speed and feed rate to lower vibration frequency.
- Use shorter tool overhang and rigid tool holders to limit deflection.
- Verify workholding stability and clamp parts with minimal overhang.
- Inspect tools for wear, damage, or imbalance before running jobs.
- Use cutting oil or mist to cool the cut and reduce thermal expansion.
What Are Chatter Marks on CNC Aluminum Parts
Chatter marks appear as parallel ridges or waviness on the surface of an aluminum part. They occur when the tool, workpiece, or machine structure vibrates during the cut. The marks can be subtle or deep enough to ruin the part. In CNC applications, these defects are common because aluminum is soft and flexible. The material deforms easily under cutting force. If the setup is not stiff enough, vibration starts.
The problem is not always the machine. It can be the tool, the fixture, or the cutting parameters. A long tool overhang can whip like a flag. A loose part can rattle against the vise. A high spindle speed can hit a resonance frequency. Each factor contributes to the same result. The part shows a pattern of ridges that repeat at a fixed distance. The distance between ridges gives a clue to the vibration source.
How to Identify the Source of Chatter
Identifying the cause requires looking at the part, the tool, and the process. The pattern of the marks matters. If the ridges are evenly spaced, the vibration is likely from the spindle or tool. If the marks are irregular, the workpiece may be loose or the fixture may be flexing. If the marks appear only in certain directions, the cutting force is exciting a structural mode.
Inspect the tool first. A dull tool rubs instead of cutting. It generates heat and vibration. A chipped edge catches on the material. The marks will be rough and uneven. A new tool often fixes the problem immediately. If the tool is fine, check the overhang. A long tool stick out from the holder creates a lever. The more overhang, the more the tool can bend. Shorten the reach where possible.
Next, check the part. Is it clamped tightly? Is there metal-to-metal contact, or is there a soft pad? Soft pads can compress under load. The part moves slightly. That movement feeds vibration back into the cut. Use hard, flat shims. Clamp the part close to the cutting area. Avoid long unsupported sections. If the part is thin, add support underneath. A thin plate can flex like a drum skin.
Common Symptoms, Causes, and Fixes
The table below lists the most common chatter scenarios. Use it as a quick check when a part shows surface defects. Match the symptom to the likely cause. Then apply the fix. This approach saves time. It avoids guessing and repeated test cuts.
| Symptom | Likely cause | What to do |
|---|---|---|
| Evenly spaced parallel ridges | Tool or spindle resonance | Lower spindle speed, shorten tool overhang, use a rigid holder |
| Irregular waviness or scallops | Loose workpiece or soft fixture | Tighten clamps, add hard shims, support the part underneath |
| Marks only on one side or in one direction | Cutting force exciting a structure mode | Reduce feed rate, change tool geometry, stiffen the fixture |
| Rough surface with deep gouges | Dull or damaged tool | Replace or sharpen the tool, check for chips |
| Vibration that changes with speed | Hitting a resonance frequency | Change the spindle speed range, reduce cutting depth, use damping |
Adjusting Cutting Parameters to Stop Vibration
Cutting parameters are the fastest thing to change. If the part is showing chatter, do not keep running. Stop and adjust. The goal is to move the cutting frequency away from the resonance of the tool and structure.
Reduce the spindle speed first. Lower speeds reduce the frequency of the vibration. The tool engages the material less often per second. The forces are smaller. The heat is lower. This is especially useful for aluminum. The material is soft. High speeds can cause it to smear or deform. A slower speed with a sharper tool often gives a cleaner surface.
Next, reduce the feed rate. A lower feed rate means each tooth engages less material. The cutting force drops. The tool deflects less. The part vibrates less. There is a trade-off. Lower feeds take longer. The cycle time increases. For a critical part, a longer run is better than a rejected part. For a high-volume job, find the sweet spot. Use the highest stable speed and feed.
Reduce the depth of cut. A shallow pass takes less force. The tool stays stiff. The part stays stable. If you need to remove a lot of material, take multiple light passes. This is slower, but it is reliable. It also helps the surface finish. A deep cut can excite a low-frequency vibration. A light cut stays above that range.
Improving Tooling and Rigidity
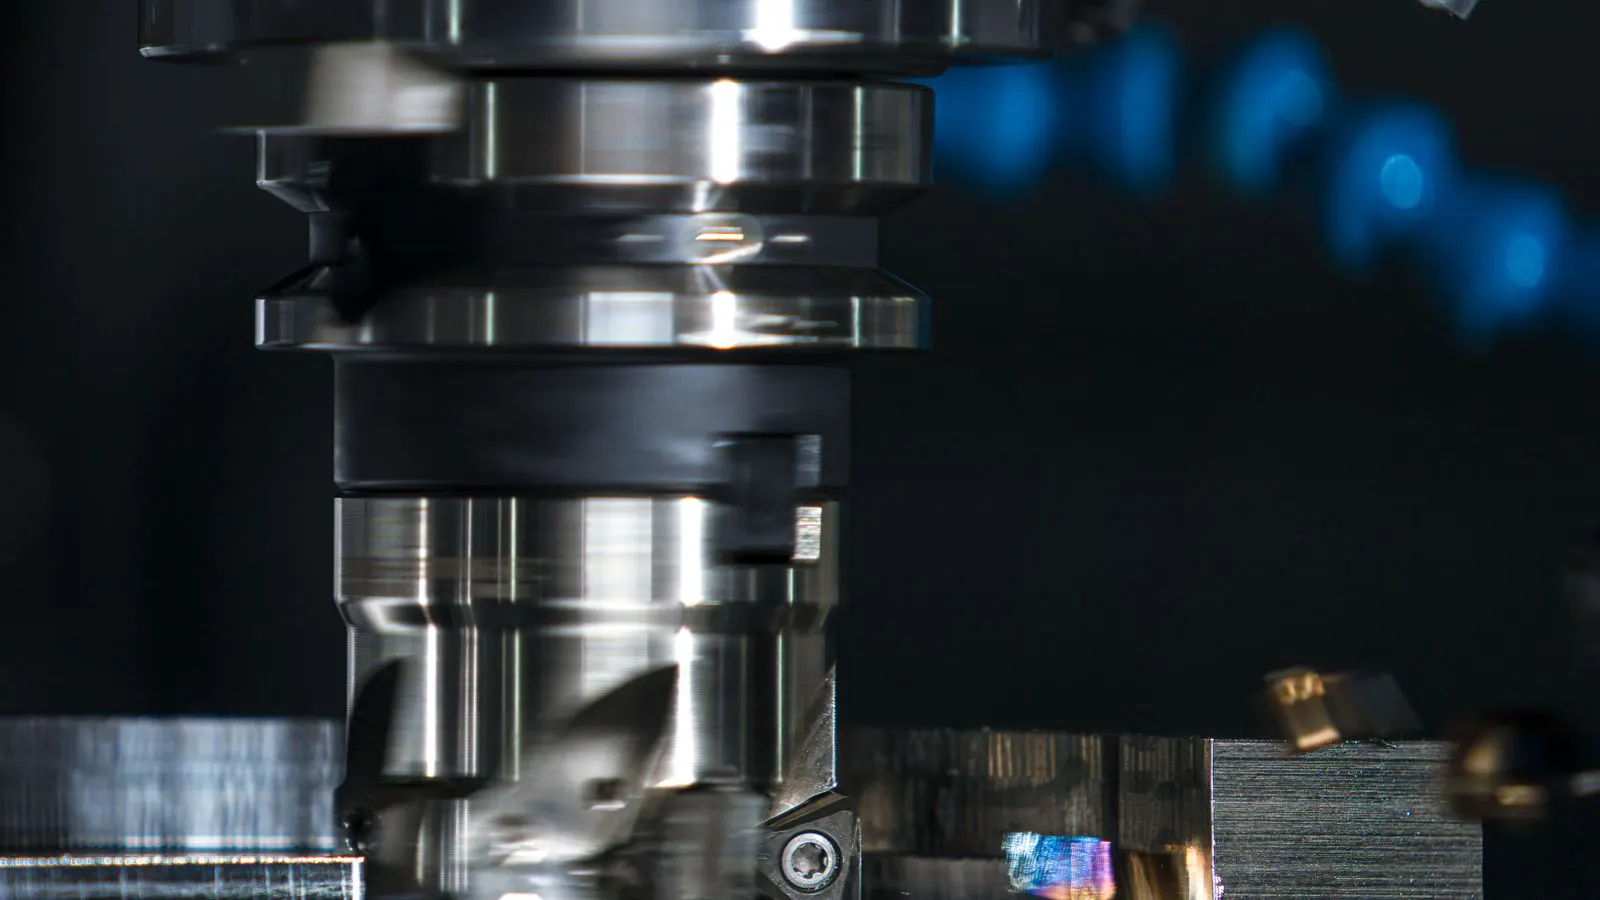
Tooling has a huge effect on chatter. The tool is the first point of contact with the material. If it is long and thin, it will bend. If it is short and thick, it will hold. Use the shortest tool possible. If the job allows, use a shorter reach. If the tool must be long, use a rigid holder. A carbide holder with a tight clamp can reduce deflection. A loose collet can allow the tool to shift. That shift creates vibration.
Check the tool geometry. A single-flute end mill can chip aluminum. The material rubs on the back of the tool. It builds heat. It vibrates. A two-flute or four-flute tool with a positive rake angle cuts cleaner. It evacuates chips better. The chip load per tooth is higher. The tool stays engaged. For aluminum, a sharp, positive geometry tool is a must.
Also check the tool holder. A worn collet can loosen over time. The tool slips slightly. That creates a micro-vibration. A broken or deformed holder can change the balance. An unbalanced tool creates a hum that can be felt in the part. Replace worn holders. Clean the tool and holder before clamping. A chip on the tool can act like a second edge. It catches and shakes.
Workholding and Fixture Stability
The part must be held like a solid block. If it is not, it will move. Even a small movement can feed energy into the vibration. Check the clamps. Are they tight? Are they in the right place? A clamp far from the cut point does not help much. The part between the clamp and the tool can still flex. Move the clamp closer to the cutting area. Add a second clamp if needed.
Use hard shims. Soft gaskets can compress. They lose their grip under load. The part shifts. The cut changes. Hard shims, such as aluminum or steel plates, maintain their position. They also distribute the clamping force. They reduce local stress. For thin parts, add a support plate underneath. The plate should be flat and rigid. It should be in contact with the bottom of the part. It should not be loose.
If the part is large, check the machine table. A long part can span across the table. The table can flex in the middle. If the part is long and thin, it can act like a beam. The vibration will be in the middle. Add a support block. It must be rigid. It must not interfere with the tool. It must be removable after the cut. For small parts, the fixture itself may be the issue. A loose fixture on the table can rock. Tighten the fixture to the table. Check for debris under the fixture.
Prevention Tips for Future Jobs
Prevention is better than repair. Chatter is a design and process problem. It is not just a machine fault. The best way to stop it is to prevent the conditions that cause it.
- Start with a low spindle speed and low feed. Run a test cut on a scrap piece. Watch the tool. Listen to the sound. A chatter sound is a high-pitched whine. It changes with the speed. If you hear it, stop and adjust.
- Use the shortest tool that can reach the cut. A long tool is a weak tool. If the job requires a long tool, use a rigid holder and a low speed.
- Clamp the part close to the cutting area. Add support underneath if the part is thin. Use hard shims to prevent compression.
- Inspect the tool for wear and damage. Replace it if it is dull or chipped. A new tool is cheaper than a rejected part.
- Keep the cutting area cool. Use cutting oil or mist. Aluminum generates heat quickly. Heat softens the material. It increases deflection. It increases chatter.
When to Change the Process
Sometimes the process itself is the problem. The part shape may be forcing a long tool. The fixture may not be able to hold it rigidly. The cutting direction may be exciting a weak mode. If the standard approach does not work, change the process.
Split the cut. Instead of one deep pass, use multiple shallow passes. This reduces the force. It reduces the vibration. It also improves the surface finish. Change the tool path. If the cut is always in the same direction, the vibration may be in that direction. Change the direction. Use a different tool. If a long end mill is causing chatter, use a ball nose or a shorter tool. If a single-flute tool is causing chatter, use a two-flute tool.
If the part is very thin, consider a different fixture. A vacuum table may be better than a vise. A vacuum holds the part from below. It does not apply a clamping force from above. It keeps the part flat. For small, thin parts, a custom fixture with multiple contact points is better than a single clamp. The part should be held at several points. This prevents flexing. It distributes the load.
Chatter is a vibration problem. It is not a mystery. It is a force problem. The forces are caused by the tool, the part, and the machine. The fix is to reduce the forces or to increase the stiffness. Reduce the cutting parameters. Stiffen the tool. Stiffen the fixture. The part will stop vibrating. The surface will be clean. The part will pass.
Frequently asked questions
Can I fix chatter marks with a higher spindle speed?
Usually no. A higher speed can increase the vibration frequency. It can hit a resonance point. Lower the speed first. If the speed is too low, try a different speed range.
What is the best tool for aluminum?
A sharp, positive-rake tool with two or four flutes works well. It cuts cleanly. It evacuates chips. It generates less heat than a dull or negative-rake tool.
How do I know if the part is loose?
Look for irregular marks. Check the clamps. Tap the part gently. If it moves, it is not rigid. Tighten the clamps. Add hard shims.
Does the depth of cut matter?
Yes. A deep cut creates high forces. It can excite vibration. Use shallow passes. Take multiple light cuts. This reduces the force. It improves the finish.
Can a machine calibration fix chatter?
Sometimes. If the machine way is worn, the structure is weaker. The vibration is more severe. A calibration can help. But the first step is always to check the tool, the fixture, and the cutting parameters.