Explainer: What is Machinable Tolerance in CNC Parts?
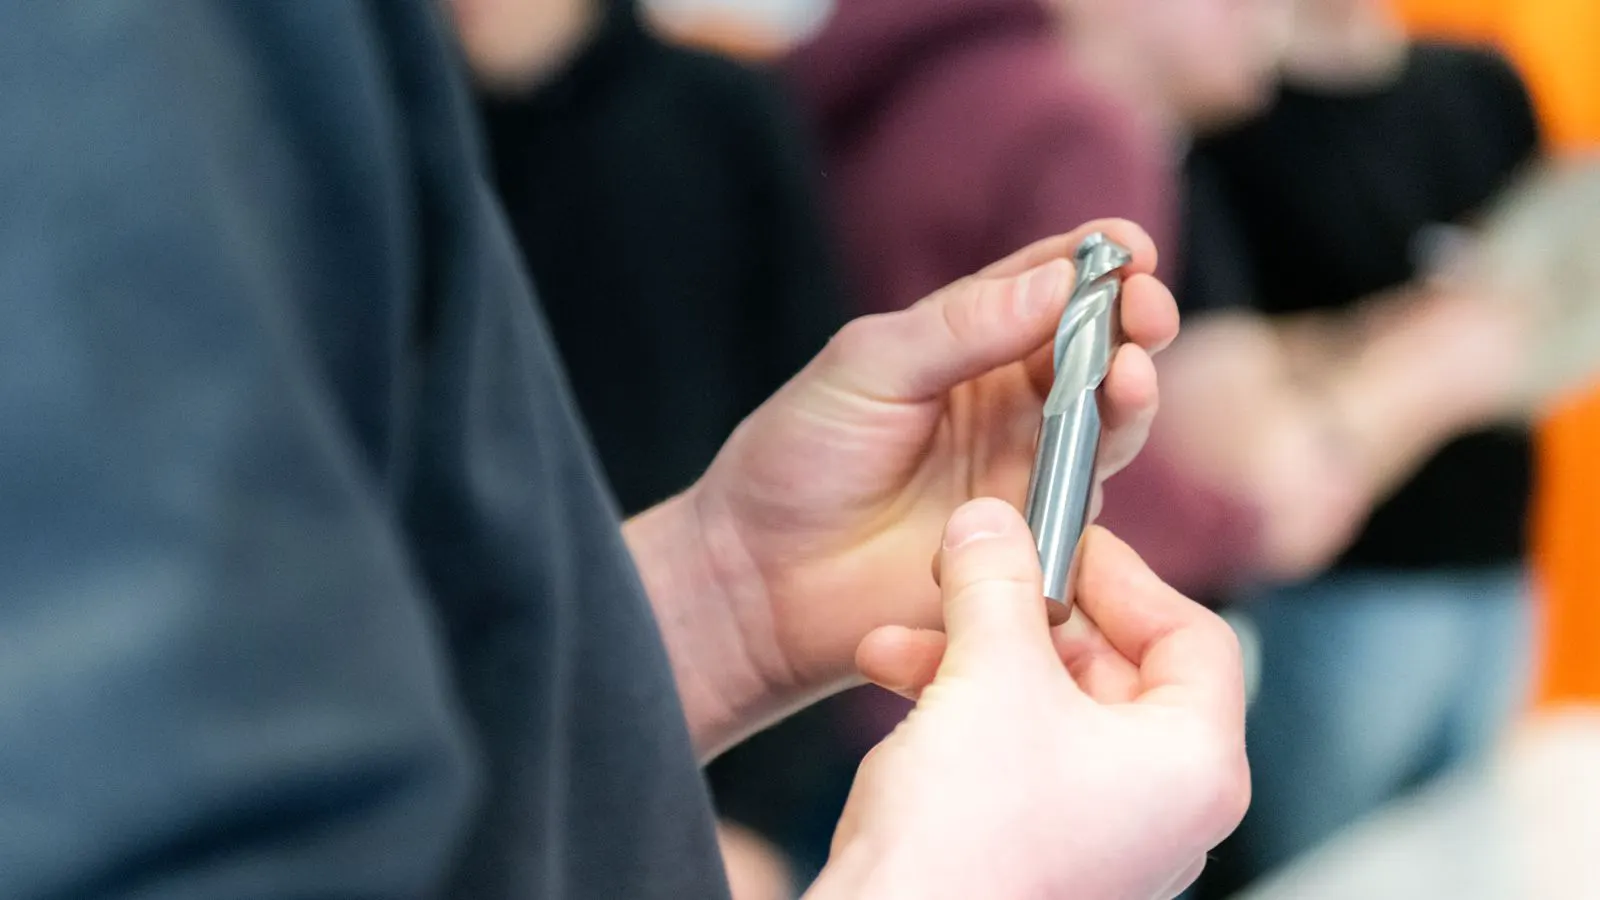
Machinable tolerance defines the minimum deviation a CNC machine can reliably hold. It depends on tooling, material, and machine class. Knowing these limits prevents over-specification and guides sourcing decisions for complex CNC parts.
- Machinable tolerance is the smallest consistent dimensional deviation a CNC process can achieve.
- The limit depends on machine class, tooling, material, and setup, not just the machine spec sheet.
- Designers should set tolerances based on function, not machine capability, to avoid unnecessary cost.
- Sourcing decisions improve when drawings specify tolerances that match realistic machining limits.
- A worked example shows how a shaft fit tolerance affects tool selection, inspection, and cost.
What is machinable tolerance in CNC machining?
Machinable tolerance is the smallest consistent dimensional deviation a CNC process can reliably hold under normal production conditions. It is not a single number. It changes with machine class, tooling, material, fixture, and the operator’s setup discipline. A part designed to hold a tolerance below the practical limit of the chosen process will fail inspection, require rework, or never be produced at scale.
This limit is distinct from the machine’s rated accuracy. Rated accuracy describes the machine’s best-case capability under ideal test conditions. Machinable tolerance describes what a shop can deliver repeatedly on a real part with real fixtures and real wear. For buyers and engineers, this distinction is what separates a workable drawing from a problem drawing.
How do CNC tolerances differ from theoretical limits?
Theoretical limits describe what physics and machine geometry allow in a perfect scenario. Machinable tolerances are the practical floor after accounting for tool deflection, thermal growth, fixture error, and operator variability. A high-end 5-axis mill can hold much tighter tolerances than a 3-axis vertical mill, but both have practical limits that depend on the specific setup.
CNC tolerances also vary by feature type. A flat surface is easier to hold than a small bore. A long shaft is harder to keep straight than a short block. A thin wall bends under cutting force in a way a thick plate does not. The same machine that holds a 0.002-inch tolerance on a large face may struggle to hold that same tolerance on a 3mm bore in hardened steel.
What factors set the machinable limit for a given part?
Several factors interact to set the practical limit. Material hardness and elasticity determine tool deflection and springback. A soft aluminum part is easier to hold than a hardened tool steel part at the same nominal tolerance. Tool size and stiffness matter. A large end mill with a short stick-out cuts more predictably than a small tool reaching deep into a pocket. Fixture rigidity affects every cut. A loose vise or a worn dowel pin introduces error that no amount of machine accuracy can correct.
Thermal behavior is another factor. Machines warm up as they run. Coolant temperature, ambient temperature, and material expansion all shift dimensions during a build. Shops that manage thermal equilibrium more consistently can hold tighter tolerances than shops that do not. This is why the same part may inspect differently on Monday morning and on Friday afternoon if the shop has not stabilized.
How does machinable tolerance affect sourcing decisions?
When a buyer sends a drawing to multiple suppliers, the tolerance stack-up determines who can quote it and at what cost. A part with aggressive tolerances on every feature pushes the quote up sharply. Each tolerance above a practical threshold adds inspection time, rework risk, or the need for a higher-end machine. The buyer may end up paying for a 5-axis machine when a 3-axis mill with a good fixture would have worked.
Sourcing decisions also depend on volume. A one-off prototype can tolerate a more expensive setup. A production run of 5000 units demands a process that can hold the tolerance repeatably without constant rework. The supplier with the right fixture, the right tooling, and the right inspection method will quote a lower unit price than the supplier who has to over-engineer the setup to hold a tolerance that is not functionally required.
Buyers should review drawings before release. A drawing that specifies 0.001-inch tolerances on decorative features, non-critical holes, and cosmetic surfaces will cost more than the function requires. Removing unnecessary tight tolerances reduces quote spread, improves yield, and makes it easier to find a capable supplier at a sustainable price.
How do machinable limits relate to inspection and acceptance?
A part that is machined within its stated tolerance must still pass inspection. The inspection method must be capable of detecting the tolerance. If the drawing calls for 0.002-inch positional tolerance, the shop needs a CMM or a dedicated fixture with the same or better capability. A micrometer cannot verify a 0.002-inch bore depth in a deep hole. A CMM can.
Inspection capability also affects sourcing. A supplier that can hold the tolerance but cannot verify it is a poor choice for a regulated or high-reliability application. The buyer should specify the inspection method or require a first-article report that demonstrates the capability. This prevents a situation where parts are accepted based on a method that cannot detect the deviation the drawing forbids.
Worked example: A shaft fit tolerance in a CNC application
Consider a machined steel shaft that must fit into a bearing bore with a clearance fit. The drawing calls for a shaft diameter of 25.00 mm with a tolerance of plus or minus 0.005 mm. The bearing bore is held to a standard tolerance that allows a light interference or light clearance fit depending on the bearing series. The shaft tolerance is tight because the bearing must spin smoothly without excessive play.
A typical CNC mill can hold this tolerance on a soft steel shaft with a standard setup. The shop uses a two-jaw chuck, a carbide tool with a short stick-out, and a coolant that keeps the workpiece and tool at a stable temperature. The first cut leaves a small finishing allowance. The second pass removes the allowance and establishes the final diameter. The shop measures with a bore gauge or a CMM and records the result.
If the drawing had called for plus or minus 0.001 mm instead, the same setup might still work on a one-off prototype. For a production run, the shop would need a more rigid fixture, a higher-grade tool, tighter thermal control, and possibly a finishing operation such as lapping or grinding. The unit cost would rise. The yield would drop because more parts would fall outside the tighter window. The buyer would need to justify the cost with a functional requirement.
If the bearing fit is actually a standard fit that allows a 0.02 mm tolerance, the drawing should say so. The machinable limit is not a ceiling. It is a floor. Designers should set tolerances at the tightest value that still meets function, then let the machinable limit guide the sourcing decision.
How should engineers set tolerances to match machinable limits?
Engineers should start with function, not capability. A gear mesh requires a tight profile tolerance. A mounting hole for a bolt requires a standard fit. A decorative surface finish requires a cosmetic tolerance. Each feature has a functional minimum. The engineer sets the tolerance at that minimum, not at the machine’s best capability.
The drawing should group features by tolerance class. A drawing that mixes 0.001-inch and 0.05-inch tolerances on the same part is harder to quote and harder to inspect. A drawing that uses standard tolerance blocks, with tighter tolerances only where function demands them, is easier to source and easier to verify.
The supplier should confirm the machinable limit during the quote stage. If the shop says the tolerance is at the edge of its capability, the buyer should ask whether a fixture change, a tool change, or a process change would improve yield. This conversation is normal. It is not a negotiation over capability. It is a conversation over risk. The buyer who understands machinable tolerance can make that conversation productive instead of adversarial.
What mistakes do buyers make with machinable tolerance?
The most common mistake is specifying a tolerance that no one needs. A buyer copies a drawing from a previous project and does not review the tolerance stack-up. The old drawing was designed for a different machine, a different material, or a different function. The new part inherits tolerances that do not fit its requirements.
Another mistake is ignoring the relationship between tolerance and surface finish. A tight tolerance and a high surface finish on the same feature are harder to achieve than either one alone. A buyer who asks for a mirror finish and a 0.001-inch dimension on the same surface is asking for two difficult things simultaneously. The quote will reflect that difficulty.
A third mistake is not defining the datum scheme. A tolerance is only meaningful relative to a datum. A hole position tolerance without a defined datum is a guess. The shop may interpret the datum in a way that is too loose for the assembly. The buyer should specify the datum scheme clearly and review it with the supplier before release.
These mistakes are not signs of incompetence. They are signs of a process gap. The fix is a review step. A single pass of the drawing with an experienced machinist or a CNC applications specialist can catch tolerance errors before they become cost overruns or production delays.
How do CNC applications vary by industry?
Different industries use CNC applications with different tolerance expectations. Medical device parts often require tight tolerances because the part must fit within an assembly that is regulated. Automotive parts may require tighter tolerances on mating surfaces but are more forgiving on decorative features. Aerospace parts may require the tightest tolerances of any industry because the cost of failure is highest.
The tolerance requirement in each case is driven by function and regulation, not by the desire to use the most precise machine available. A medical device part that does not need a 0.001-inch tolerance should not be specified with one. An automotive part that needs a 0.05-inch hole position should not be specified with a 0.001-inch tolerance. The CNC applications that work best are the ones where the tolerance matches the function.
Buyers in regulated industries should also consider the inspection and documentation requirements. A part that passes the tolerance may still fail the audit if the inspection record is incomplete. The CNC applications in those industries require a chain of evidence from the machine to the final report. The buyer should specify the documentation requirement in the drawing or the purchase order.
How do you verify that a supplier can hold the machinable tolerance?
Verification starts with a first-article inspection. The supplier machines one part and inspects it against the drawing. The buyer reviews the report. If the part passes, the process is capable. If the part fails, the shop must explain the deviation and provide a corrective action. This is not a formality. It is the first real test of whether the machinable limit is real.
For production runs, the buyer should require periodic verification. A part that passed the first article may drift if the tool wears, the fixture loosens, or the material changes. A periodic inspection catches drift before it becomes a batch failure. The buyer should agree on the inspection frequency with the supplier before release.
The buyer should also ask about the supplier’s capability beyond the current part. If the drawing calls for a tolerance that is at the edge of the supplier’s capability, the supplier may be able to hold it, but the yield may be low. The buyer should ask for a yield estimate or a historical performance reference. This information helps the buyer decide whether to accept the risk or to move the part to a different supplier with more headroom.
What is the practical takeaway for sourcing CNC parts?
The practical takeaway is this: machinable tolerance is a design input, not a machine output. The buyer and the engineer set the tolerance based on function. The supplier confirms that the tolerance is within its machinable limit. The inspection method verifies the tolerance. The documentation records the verification. This chain is what makes a CNC part reliable.
A buyer who understands this chain can source parts at a lower cost, with less risk, and with higher yield. The buyer who does not understand this chain will overpay, over-specify, and over-inspect. The difference is not technical. It is practical. It is the difference between a part that works and a part that causes problems.
The CNC applications that succeed are the ones where every tolerance has a reason. Every inspection has a method. Every supplier has a capability. The machinable tolerance is the thread that connects all three. It is the smallest deviation that the process can hold, the tightest value that the function requires, and the practical floor for the part. Understanding that floor is the first step toward reliable sourcing.
Frequently asked questions
What is the difference between rated machine accuracy and machinable tolerance?
Rated machine accuracy describes the best-case capability of the machine under ideal test conditions. Machinable tolerance describes what the shop can deliver repeatedly on a real part with real fixtures, tools, and material. The machinable tolerance is usually tighter or looser than the rated accuracy depending on the setup.
How tight can CNC machining go?
It depends on the machine class, tooling, material, and fixture. A high-end 5-axis mill can hold much tighter tolerances than a standard 3-axis mill. But even the best machines have practical limits. The machinable limit is not a single number. It changes with every setup.
Should I specify the tightest tolerance I can afford?
No. Specify the tightest tolerance that meets function. Tighter than function costs more, reduces yield, and makes sourcing harder. A tolerance that is not functionally required is a cost with no benefit.
How do I know if my drawing has unrealistic tolerances?
Send the drawing to a supplier and ask for a capability review. If the supplier says a tolerance is at the edge of its capability, ask for a first-article inspection before production. A tolerance that causes rework on the first part will cause rework on every part.
Does the material affect machinable tolerance?
Yes. Soft materials like aluminum are easier to hold than hardened steels. The tool deflection, springback, and thermal behavior all change with material. A tolerance that is easy to hold in aluminum may be difficult to hold in tool steel.