Outlook: Generative Design for CNC Machinability
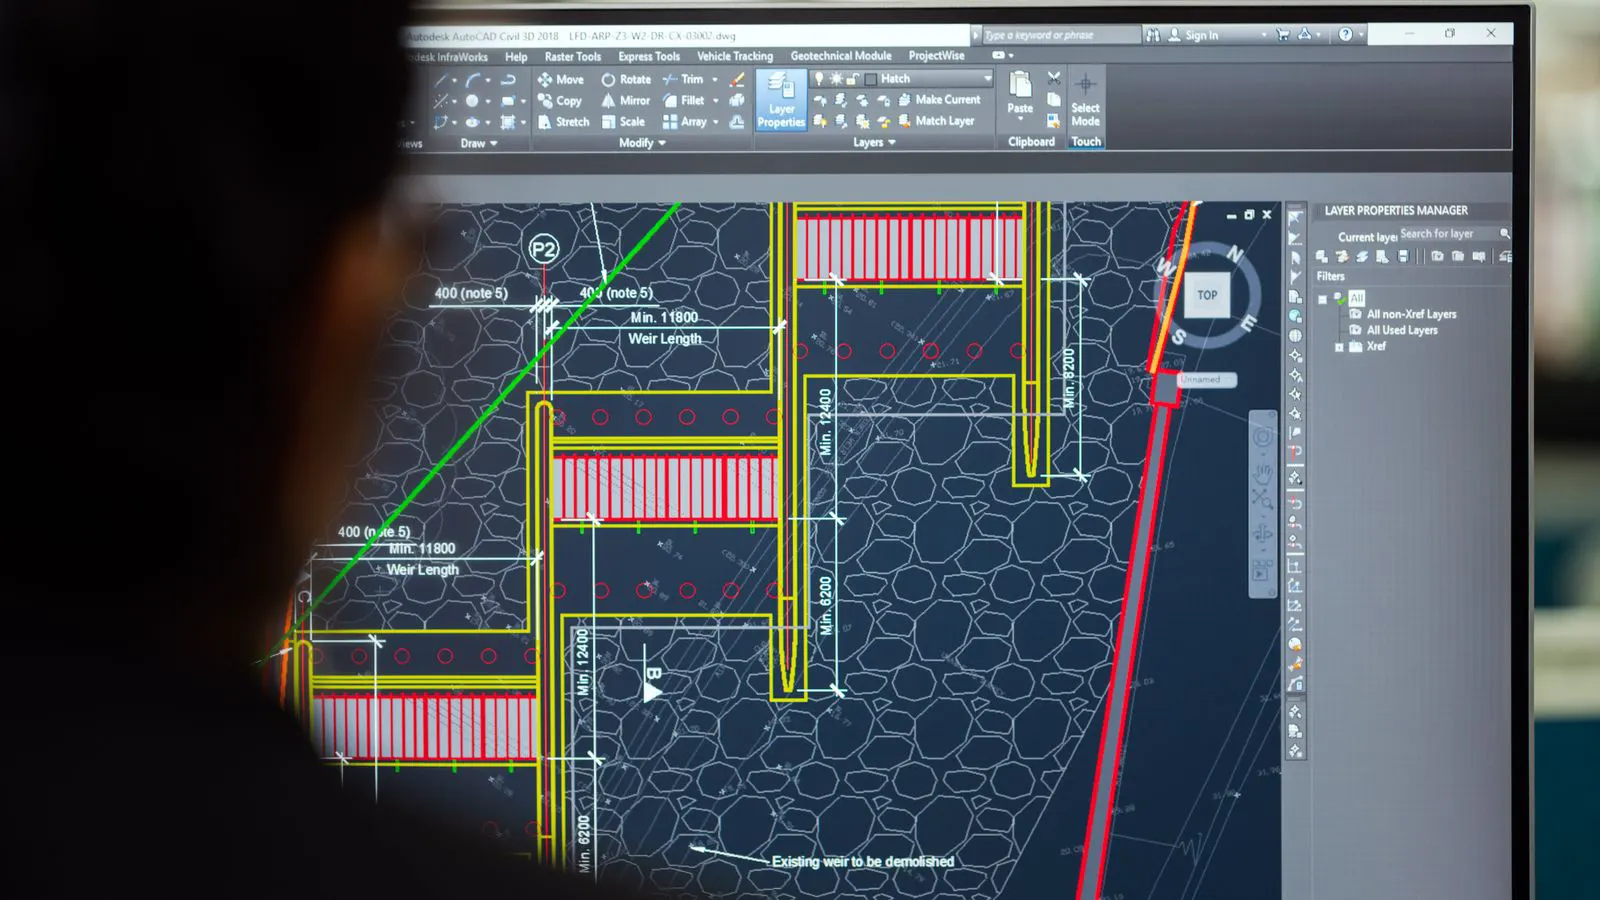
Generative design tools are shifting the focus from fixed geometry to constraint-based solutions. They require new workflows for evaluating tool access, material removal, and post-processing. Buyers should update their cnc design guidelines, pilot small projects, and align engineering and manufacturing teams early to reduce rework and cost.
- Generative design shifts the burden from fixed geometry to constraint-based solutions.
- New workflows are needed to evaluate tool access, material removal, and post-processing.
- Buyers should update cnc design guidelines and pilot small projects to reduce rework.
How Generative Design Changes the Starting Point
Generative design tools start from performance requirements rather than a fixed shape. Instead of drafting a bracket or housing with traditional solid modeling, an engineer defines load paths, mounting points, material limits, and manufacturing constraints. The software then proposes multiple geometry options that satisfy those rules. The result is often a structure that looks unlike anything a designer would sketch by hand.
For CNC shops, this shift changes the first question in a quote request. The buyer no longer asks if a drawing is manufacturable. The buyer asks if a set of constraints can be satisfied without excessive setup complexity. The part itself is no longer fixed before the shop is involved. It is a variable in an optimization loop.
This is why dfm for cnc is moving from a late-stage drawing review to an early-stage design input. The shop is no longer just checking a finished model for tool clearance. The shop is helping define the boundaries within which the algorithm can search.
What Changes in Part Geometry
The most visible shift is in geometry. Generative outputs often use organic, lattice-like, or variable-thickness structures. These shapes look unusual but are driven by load distribution. A solid block of aluminum or stainless steel is replaced by a structure that removes material where stress is low.
This creates a direct conflict with traditional cnc part design. A solid block is easy to mill. It has flat faces, predictable tool paths, and minimal risk of thin-walled failure. A generated lattice structure may have small internal channels, variable wall thickness, and sharp internal corners. These features can be difficult for a standard end mill to reach without breaking the tool or leaving unmachined material.
Buyers should expect to see more thin-walled parts in the future. Thin-walled parts are common in aerospace and medical applications where weight savings are required. CNC milling can produce them, but they demand careful tool selection and cutting strategy. The generative output may include features that are impossible to machine with a conventional 3-axis setup.
How Constraint-Based Design Affects Tool Access
Tool access is the most immediate friction point between generative design and CNC machining. A traditional part has defined pockets and slots. A generated part may have internal voids that are only accessible from one or two directions. The algorithm may optimize for weight without considering the angle at which a cutter can enter the space.
This is where cnc design guidelines must evolve. The old guidelines focused on draft angles, minimum wall thickness, and standard hole sizes. The new guidelines must include tool diameter limits, approach angles, and clearance volumes. If a generated feature requires a 1/4 inch tool to reach a 1/2 inch internal radius, the part is not manufacturable without a special fixture or a 5-axis process.
Buyers should ask their software vendor how manufacturing constraints are weighted in the optimization. A model that prioritizes weight may produce a structure that is impossible to machine. A model that prioritizes manufacturability may produce a heavier part. The balance between these two objectives is a business decision, not just an engineering one.
The Role of Fixturing in Complex Geometries
Complex geometry creates fixturing challenges that do not exist in traditional part design. A generated part may have no flat, stable surfaces for clamping. It may have rounded outer contours that make it difficult to hold in a vise. It may require vacuum tables, custom soft jaws, or 5-axis simultaneous machining to hold it in place.
This is why How to Design CNC Parts for Easier Fixturing remains a relevant topic even as design tools become more advanced. Fixturing is not a separate step. It is an integral part of the machining strategy. If a part cannot be held securely during cutting, the generative design is a failure, regardless of how efficient the load path is.
Buyers should plan for custom fixturing costs in their budget. A standard vise setup may not work for every generated part. The shop may need to machine a dedicated fixture for each part type. This adds setup time and cost. It also adds complexity to the production schedule.
How Material Selection Interacts with Generated Structures
Material selection is no longer a simple choice between aluminum, steel, or titanium. The material properties must be matched to the specific load paths generated by the software. A titanium part may be chosen for weight and strength, but the tooling requirements are higher than for aluminum. A steel part may be chosen for durability, but the material removal rate is lower.
The generative algorithm may optimize for a material that is not economically viable for the required production volume. A buyer might get a design that uses a high-alloy steel for a prototype, but that material is too expensive for a batch of five hundred units. The material choice must be reviewed against the production plan, not just the performance requirements.
This is where manufacturability tips become more nuanced. The buyer should ask if the generated structure is compatible with the available tooling. If the part requires a carbide tool with a small diameter, the tool life may be short. If the part requires a 5-axis mill, the cycle time may be long. The material and the geometry must be evaluated together.
| Design Factor | Traditional Approach | Generative Approach |
|---|---|---|
| Geometry | Fixed, solid shapes | Variable, organic structures |
| Tool Access | Predictable pockets | Variable internal voids |
| Fixturing | Standard flat surfaces | Custom or 5-axis required |
| Material Selection | Based on function | Based on load path and cost |
| Post-Processing | Standard deburring | Complex internal cleaning |
What Buyers Should Do to Prepare
Buyers cannot wait for the technology to mature before adapting their workflows. The shift is already happening. The question is whether the buyer is ready to integrate these tools into their process.
- Update cnc design guidelines to include tool diameter limits and approach angles.
- Involve the machining shop in the early constraint definition phase.
- Pilot generative design on low-risk, low-volume parts to test the workflow.
- Review fixturing and post-processing costs alongside the material cost.
- Establish a feedback loop between the shop and the design team.
The first step is to define the constraints clearly. The buyer must tell the software what is allowed and what is not. This includes maximum tool diameter, minimum wall thickness, and available machine axes. Without these inputs, the software will produce a design that is theoretically perfect but practically unmanufacturable.
The second step is to pilot. Do not start with a critical aerospace component. Start with a non-critical bracket or a prototype housing. This allows the team to test the workflow, identify the friction points, and refine the guidelines. The pilot will reveal the gaps between the design intent and the manufacturing reality.
The third step is to review the post-processing. Generated parts often have complex surfaces that are difficult to deburr. They may have small internal channels that are hard to clean. The buyer must account for this in the final cost. The machining cost is only one part of the total cost. The finishing cost can be significant.
The Long-Term Impact on Shop Capabilities
The long-term impact will be a shift in shop capabilities. Shops that only offer 3-axis milling may find themselves unable to compete on generative design jobs. The complexity of the parts will require 5-axis machining, high-speed milling, and specialized tooling.
This does not mean that 3-axis shops will disappear. They will still be needed for simple parts, large flat parts, and standard fixtures. But the high-value work will move to shops with advanced capabilities. The buyer must decide where to place their orders based on the complexity of the generated part.
The shop that can integrate generative design into its quote process will have a competitive advantage. It can identify manufacturability issues early and suggest design changes before the part is cut. This reduces rework and shortens the time to production. The buyer benefits from lower cost and faster delivery.
The future of dfm for cnc is not just about checking drawings. It is about co-designing parts with the shop. The engineer and the machinist will work together to define the constraints and optimize the geometry. The part will be designed for the machine, not the other way around.
Frequently asked questions
Can generative design replace traditional CAD modeling?
No, it complements traditional CAD. The generated geometry still needs to be translated into a manufacturing model with defined tool paths and tolerances.
What is the biggest risk when using generative design for CNC parts?
The biggest risk is producing a geometry that is impossible to machine with standard tooling. This leads to long quote cycles and potential redesigns.
How do I know if a generated part is manufacturable?
Run a simulation or ask the shop to review the tool access and fixturing requirements. A standard 3-axis shop may not be able to produce a 5-axis generated part.
Does generative design save money on parts?
It can reduce material cost by removing unnecessary mass. However, it may increase machining and post-processing costs. The total cost depends on the balance.
What should I include in my cnc design guidelines for generative parts?
Include tool diameter limits, approach angles, minimum wall thickness, and available machine axes. These constraints help the software produce manufacturable geometry.