CNC Wall Thickness Rules: Avoiding Costly Failures
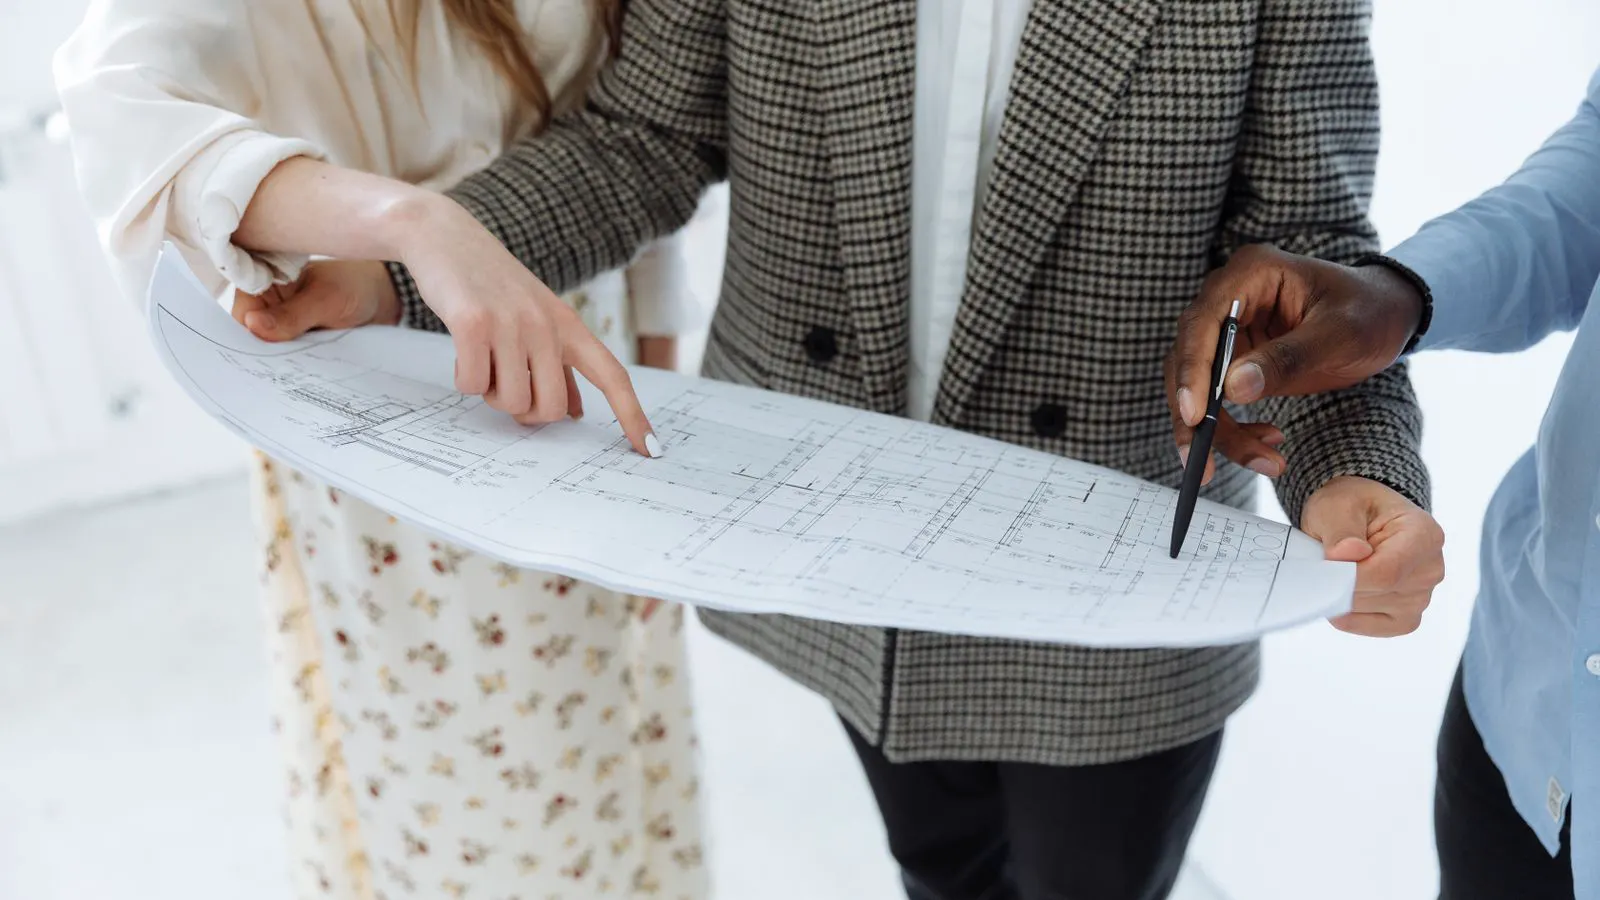
Minimum wall thickness depends on material, size, and process. Follow these practical CNC design guidelines for thin wall machining to prevent collapse, vibration, and expensive rework.
- Minimum safe wall thickness varies by material, part size, and whether the part is machined or turned.
- Check for collapse points, vibration zones, and heat distortion before releasing a drawing for manufacturing.
- Add DFM notes to drawings to flag thin walls and agreed tolerances.
- Plan for fixture clearance and tool access in every wall thickness review.
- Use generative design and DFAM software to catch thin wall issues before CAD release.
A thin wall can save weight and material. It can also cost a shop weeks of rework. The failure rarely looks dramatic. A part may arrive with a hairline crack, a warped face, or a wall that simply buckled under the pressure of a fixture. For buyers, the problem is that these defects are often invisible until the part is on the machine or on the test bench.
These are the design rules that keep thin walls from becoming expensive problems.
What is the minimum wall thickness for a CNC part?
There is no single number. A 1 mm wall in mild steel behaves differently from a 1 mm wall in 7075 aluminum. A part 50 mm across needs more support than a part 500 mm across. The rule of thumb is to start with the thinnest wall that the material, size, and process can handle without collapse or vibration.
For many machined parts, a starting point is 1.5 to 2 mm for small parts in aluminum or plastics, and 3 to 5 mm for large parts or steels. These are starting points, not guarantees. A machinist will tell you that a 1 mm wall on a small bracket can be machined without issue if the fixture is right. The same wall on a large plate will chatter and fail.
The material matters. Aluminum is forgiving. It bends before it breaks. That can save a part from a crack, but it can also leave a deformed surface that fails dimensional checks. Steels are stiffer but more brittle. A thin steel wall may hold shape but crack under fixture pressure.
Size matters too. A large, thin plate needs stiffening ribs. A small, thin tube needs support at the ends. A part with a long, unsupported wall will deflect under its own weight.
How do you prevent thin wall collapse?
Collapse happens when a wall is pushed beyond its limit. The causes are usually one of three things: fixture pressure, cutting forces, or heat.
Fixture pressure is the most common. A part sits on a vise or a fixture plate. The operator tightens the clamp. A thin wall bends. If the part is small, the bend may be small. If the part is large, the bend can exceed tolerance.
The fix is to change how the part is held. Use vacuum pads. Use a conforming fixture. Add support features to the part design. A small rib, a boss, or a pocket can change the bending behavior entirely.
The design team should review the fixture plan with the shop. A drawing with a thin wall and no fixture notes is an invitation to failure. Add DFM notes to the drawing. Mark the thin walls. Specify the tolerance. State the material. Flag the areas that need special holding.
Cutting forces can also collapse a wall. A large tool takes a deep cut. The chip pushes the wall. The wall deflects. The tool follows the deflected path. The part is out of tolerance.
The fix is to reduce the cut per pass. Use a smaller tool. Add a back-up pass. Machine from both sides if possible. The design team can help by avoiding deep pockets in thin walls. A shallow, wide pocket is easier to hold than a deep, narrow one.
Heat can soften a wall. Aluminum is especially sensitive. A long cut path heats the part. The part expands. The tool follows the expanded path. The part cools. The part is out of tolerance.
The fix is to use coolant. Use a smaller tool. Take shorter cuts. The design team can help by avoiding long, continuous cuts in thin walls. Break the cut into shorter segments. Add relief pockets.
What tolerances should you specify on thin walls?
Tight tolerances on thin walls are expensive. A 0.05 mm tolerance on a 1 mm wall is harder to hold than a 0.05 mm tolerance on a 10 mm wall. The wall flexes. The tool deflects. The part moves.
A practical approach is to use a looser tolerance on thin walls. A 0.1 mm tolerance on a 1 mm wall is often acceptable. A 0.05 mm tolerance on a 10 mm wall is easier to hold.
The design team should review the tolerance stack-up. If three thin walls must align to a 0.05 mm tolerance, the total stack-up may be 0.15 mm. That is a problem.
The fix is to change the design. Use a single, thicker wall. Add a pin or a boss for alignment. Reduce the number of thin walls in the critical path.
DFM notes on the drawing should state the tolerance on thin walls. If the tolerance is tight, say so. If the tolerance is loose, say so. The shop will appreciate the clarity.
How do you design for thin wall machining?
The design should make the part easy to machine. A part with a 1 mm wall and a 10 mm deep pocket is a bad part. A part with a 1 mm wall and a 2 mm deep pocket is a good part.
The design team should review the part for tool access. Can a 6 mm tool reach the pocket? Can a 3 mm tool reach the corner? If not, the design needs to change.
The design team should review the part for fixture clearance. Can the part sit flat on the machine table? Can the clamps reach the part without hitting the thin wall? If not, the design needs to change.
The design team should review the part for heat. Can the part be cooled during machining? Can the part be supported to prevent heat buildup? If not, the design needs to change.
A practical approach is to run the part through a DFAM software package. The software will flag thin walls. It will flag tight tolerances. It will flag features that are hard to machine. The design team can fix the issues before the drawing is released.
How do you prepare for thin wall machining?
The buyer should plan for the thin wall review. The review should happen before the drawing is released. The review should involve the design team, the shop, and the buyer.
The review should cover the following:
- Minimum wall thickness for each material in the part.
- Tolerance on each thin wall.
- Fixture plan for each thin wall.
- Tool access for each thin wall.
- Heat management for each thin wall.
- DFM notes on the drawing for each thin wall.
The buyer should ask the shop for a DFM report. The report should list the thin walls, the tolerances, the fixture plan, and the tool access. The buyer should review the report before releasing the drawing.
The buyer should also ask the shop for a sample. A sample part is a good way to check the wall thickness and the surface finish. The sample part should be machined by the same shop that will produce the part. The sample part should be measured with the same instruments that will be used for inspection.
A practical approach is to use a generative design tool to explore the part shape. The tool will create a part with a thin wall. The design team can review the wall thickness and the tolerance. The shop can review the fixture plan. The buyer can review the cost.
How do you avoid costly rework on thin walls?
Rework is expensive. A thin wall that fails dimensional checks must be reworked. The part must be re-machined. The part must be re-inspected. The part must be re-packed. The cost is real.
The fix is to get the design right the first time. The design should be reviewed with the shop. The drawing should have DFM notes. The shop should provide a DFM report. The buyer should review the report before releasing the drawing.
A practical approach is to use a DFAM software package to review the part. The software will flag the thin walls. The software will flag the tight tolerances. The software will flag the features that are hard to machine. The design team can fix the issues before the drawing is released.
The buyer should also ask the shop for a sample part. The sample part is a good way to check the wall thickness and the surface finish. The sample part should be machined by the same shop that will produce the part. The sample part should be measured with the same instruments that will be used for inspection.
The table below shows a practical starting point for minimum wall thickness. These are starting points, not guarantees. The shop will confirm the minimum wall thickness for the specific part.
| Material | Part Size | Starting Minimum Wall |
|---|---|---|
| Aluminum | Small | 1.5 mm |
| Aluminum | Large | 3 mm |
| Mild Steel | Small | 3 mm |
| Mild Steel | Large | 5 mm |
| Stainless Steel | Small | 3 mm |
| Stainless Steel | Large | 5 mm |
The shop will confirm the minimum wall thickness. The shop will also confirm the tolerance. The shop will also confirm the fixture plan.
The buyer should plan for the thin wall review. The review should happen before the drawing is released. The review should involve the design team, the shop, and the buyer.
The buyer should also plan for the sample part. The sample part is a good way to check the wall thickness and the surface finish. The sample part should be machined by the same shop that will produce the part. The sample part should be measured with the same instruments that will be used for inspection.
The buyer should also plan for the DFM report. The DFM report should list the thin walls, the tolerances, the fixture plan, and the tool access. The buyer should review the report before releasing the drawing.
The buyer should also plan for the DFM notes. The DFM notes should be on the drawing. The DFM notes should flag the thin walls. The DFM notes should state the tolerance. The DFM notes should state the material. The DFM notes should flag the areas that need special holding.
The buyer should also plan for the generative design review. The generative design review should happen before the CAD release. The generative design review should involve the design team, the shop, and the buyer. The generative design review should flag the thin walls. The generative design review should flag the tight tolerances. The generative design review should flag the features that are hard to machine.
The buyer should also plan for the DFAM software review. The DFAM software review should happen before the drawing is released. The DFAM software review should flag the thin walls. The DFAM software review should flag the tight tolerances. The DFAM software review should flag the features that are hard to machine.
The buyer should also plan for the fixture review. The fixture review should happen before the drawing is released. The fixture review should involve the shop. The fixture review should flag the thin walls. The fixture review should flag the areas that need special holding. The fixture review should flag the areas that need support.
The buyer should also plan for the tool access review. The tool access review should happen before the drawing is released. The tool access review should involve the shop. The tool access review should flag the thin walls. The tool access review should flag the features that are hard to machine. The tool access review should flag the features that need a smaller tool.
The buyer should also plan for the heat management review. The heat management review should happen before the drawing is released. The heat management review should involve the shop. The heat management review should flag the thin walls. The heat management review should flag the features that generate heat. The heat management review should flag the features that need coolant.
The buyer should also plan for the tolerance stack-up review. The tolerance stack-up review should happen before the drawing is released. The tolerance stack-up review should involve the design team. The tolerance stack-up review should flag the thin walls. The tolerance stack-up review should flag the critical features. The tolerance stack-up review should flag the features that need a looser tolerance.
The buyer should also plan for the sample part review. The sample part review should happen before the production run. The sample part review should involve the buyer and the shop. The sample part review should check the wall thickness. The sample part review should check the surface finish. The sample part review should check the tolerance.
The buyer should also plan for the DFM report review. The DFM report review should happen before the drawing is released. The DFM report review should involve the buyer and the shop. The DFM report review should check the thin walls. The DFM report review should check the tolerances. The DFM report review should check the fixture plan.
The buyer should also plan for the DFM notes review. The DFM notes review should happen before the drawing is released. The DFM notes review should involve the buyer and the design team. The DFM notes review should check the thin walls. The DFM notes review should check the tolerances. The DFM notes review should check the material.
The buyer should also plan for the generative design review. The generative design review should happen before the CAD release. The generative design review should involve the buyer, the design team, and the shop. The generative design review should check the thin walls. The generative design review should check the tight tolerances. The generative design review should check the features that are hard to machine.
The buyer should also plan for the DFAM software review. The DFAM software review should happen before the drawing is released. The DFAM software review should involve the buyer and the design team. The DFAM software review should check the thin walls. The DFAM software review should check the tight tolerances. The DFAM software review should check the features that are hard to machine.
The buyer should also plan for the fixture review. The fixture review should happen before the drawing is released. The fixture review should involve the buyer and the shop. The fixture review should check the thin walls. The fixture review should check the areas that need special holding. The fixture review should check the areas that need support.
The buyer should also plan for the tool access review. The tool access review should happen before the drawing is released. The tool access review should involve the buyer and the shop. The tool access review should check the thin walls. The tool access review should check the features that are hard to machine. The tool access review should check the features that need a smaller tool.
The buyer should also plan for the heat management review. The heat management review should happen before the drawing is released. The heat management review should involve the buyer and the shop. The heat management review should check the thin walls. The heat management review should check the features that generate heat. The heat management review should check the features that need coolant.
The buyer should also plan for the tolerance stack-up review. The tolerance stack-up review should happen before the drawing is released. The tolerance stack-up review should involve the buyer and the design team. The tolerance stack-up review should check the thin walls. The tolerance stack-up review should check the critical features. The tolerance stack-up review should check the features that need a looser tolerance.
The buyer should also plan for the sample part review. The sample part review should happen before the production run. The sample part review should involve the buyer and the shop. The sample part review should check the wall thickness. The sample part review should check the surface finish. The sample part review should check the tolerance.
The buyer should also plan for the DFM report review. The DFM report review should happen before the drawing is released. The DFM report review should involve the buyer and the shop. The DFM report review should check the thin