Fixing Common CNC Turning Vibration and Surface Finish Issues
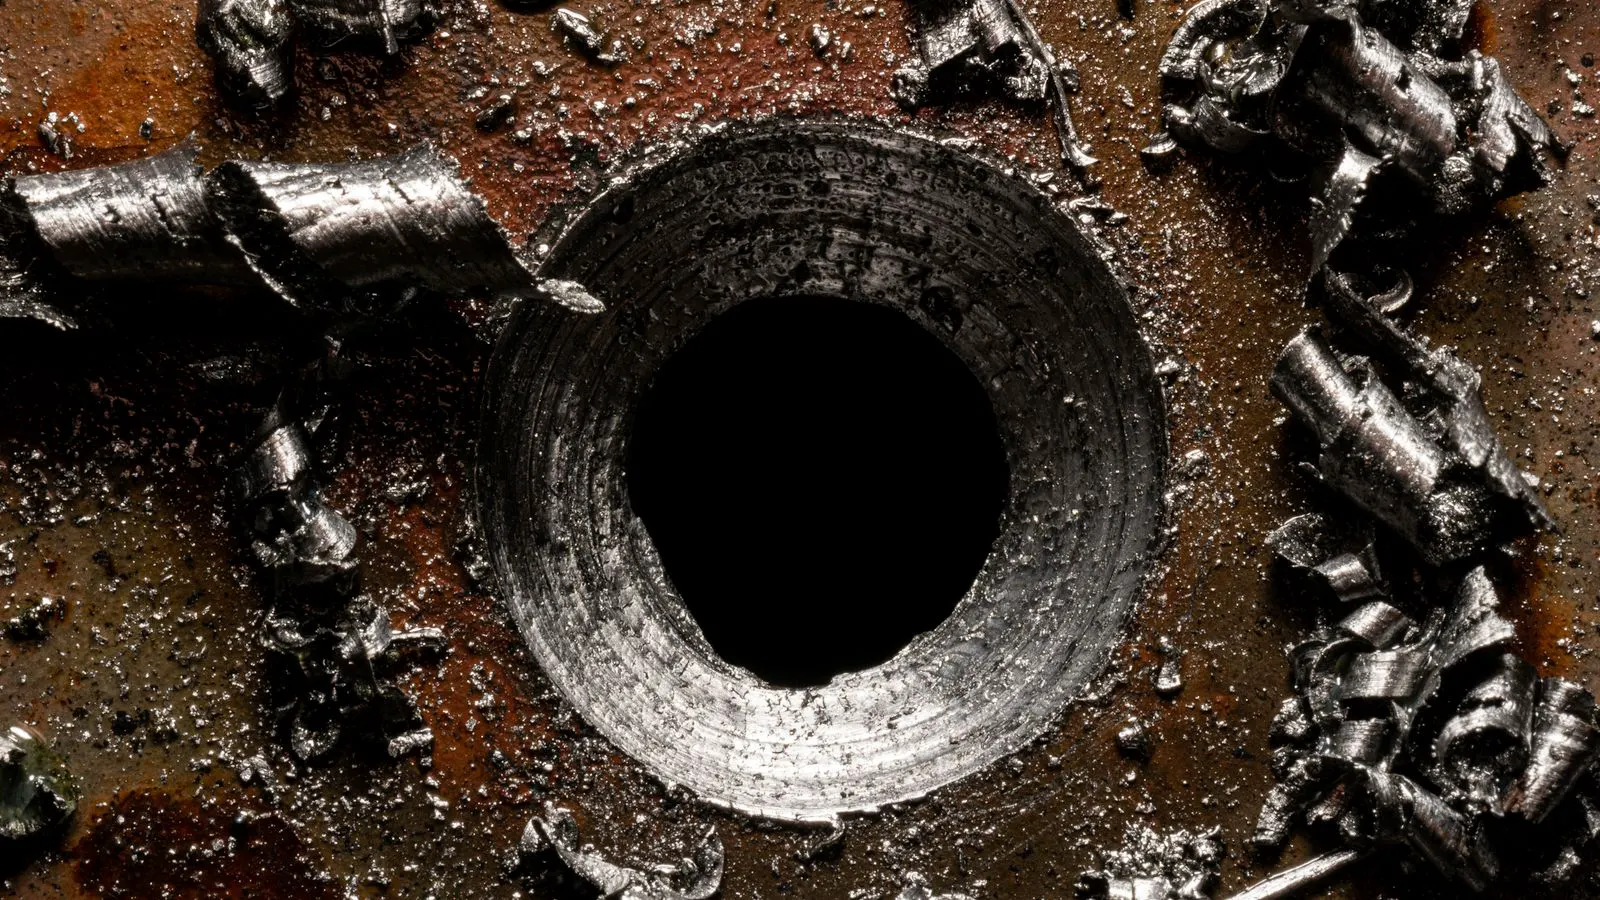
Poor surface finish in CNC turning is rarely a mystery. Most chatter traces back to weak rigidity, wrong tool geometry, or unstable cutting parameters. This guide maps each symptom to its cause and gives practical fixes to restore a clean finish.
- Check tool overhang and rigidity before adjusting feed rates.
- Match cutting parameters to the tool holder and machine stiffness.
- Use high-rigidity tooling and reduce overhang to dampen chatter.
- Inspect workholding and tooling for looseness before every run.
- Keep cutting speeds and feeds within the tooling and machine limits.
What does CNC turning vibration actually look like
Chatter on a lathe leaves a telltale mark. The finished surface shows a regular ripple pattern, often with a spacing that matches the tool or spindle frequency. The marks can look like shallow grooves or a wavy texture running across the part. In severe cases, the tool skips, the surface becomes rough, and the part may fail dimensional checks even if the diameter looks close.
Engineers often blame the program first. The program is usually not the problem. If the tool, holder, and workholding are stable, the same G-code will cut cleanly. If the system is loose or poorly matched, the same program will chatter in aluminum, steel, or titanium. The first step is to identify where the energy is entering the system and where it is escaping.
Common symptoms and their likely causes
The table below maps the most common turning vibration symptoms to their usual causes and the fixes that work in practice.
| Symptom | Likely cause | What to do |
|---|---|---|
| Regular ripple marks on finished surface | Tool overhang, weak tool holder, or unstable cutting parameters | Reduce overhang, tighten holder, lower feed or raise speed within tool limits |
| Rough surface only at start or end of cut | Workpiece not fully supported, tool entering from a weak zone | Add a steady rest or support bar, verify workholding |
| Chatter that changes with depth of cut | Machine or tool deflection near the limit of stiffness | Reduce depth of cut, use a stiffer tool, or add support |
| Vibration only at high speed | Tool geometry mismatch or unbalanced tooling | Check tool balance, reduce speed, verify tool orientation |
| Surface finish varies along the part | Tool wear or inconsistent workholding pressure | Replace or recondition tool, recheck clamp torque and alignment |
Start with the tool. If the holder is loose or the overhang is longer than necessary, no program will save the cut. If the tool itself is worn or the wrong geometry for the material, the cut will never be clean.
How to reduce tool overhang and holder deflection
Overhang is the first thing to check. A tool sticking out far from the holder creates a long lever arm. Even a small radial deflection becomes a big vibration at the cutting edge. For a standard turning operation, keep the tool as close to the holder as the machine allows. If the holder position is fixed, use a shorter insert or a holder with a smaller nose radius.
A rigid holder is the next step. A tool that is loose in the holder will chatter before the cut even starts. Check the clamping force and make sure the insert is seated properly. If the holder is old or worn, it may flex even when it looks tight. A new holder or a tool with a shorter shank often solves the problem immediately.
Do not over-tighten. Too much clamping force can distort the holder or the tool shank, which changes the cutting edge position and can create a new kind of vibration. Use the manufacturer’s recommended torque and check it after the first few cuts.
Cutting parameters that cause chatter
Feed rate and cutting speed interact with tool stiffness. A high feed rate can push the tool into a deflection zone where the cutting edge jumps from one surface to the next. A low speed can make the tool rub instead of cut, especially in harder materials. The fix is usually to move within the tool’s recommended range rather than to push the machine to its limits.
If the current feed rate is producing a rough finish, try lowering it slightly and raising the speed within the tool’s limits. This reduces the force per cut and lets the tool remove material more evenly. If the speed is already at the top of the recommended range, lower the speed and adjust the feed to match. The goal is a clean cut, not the fastest cycle.
For thin-walled parts, reduce the depth of cut and use a lighter feed. Thin parts have less stiffness than solid stock. A small depth of cut keeps the tool from flexing the workpiece into a vibration zone. If the part is already thin, support it with a steady rest or a backing plate.
Workholding and setup checks
A loose workpiece will chatter even with a perfect tool. Check the chuck jaws or collet for wear and make sure the part is centered. A part that is not centered will hit the tool at an uneven angle, creating a pulsing force. A part that is not fully supported will flex between supports, especially if the overhang is long.
Use a steady rest for long bar stock. A steady rest supports the workpiece without adding friction to the surface. It also keeps the tool from deflection into the unsupported section. If the part is hollow, use an internal support or a back bar to prevent the wall from bowing.
Clamp torque matters. A part that is not clamped hard enough will shift during the cut. A part that is clamped too hard can deform, especially in soft materials. Use the correct torque for the material and check it after the first cut. If the part is soft, use a backing plate or a fixture that distributes the clamp force.
Tooling and insert selection
The wrong tool for the job will chatter. For roughing, a tool with a larger nose radius and a steeper rake angle can handle higher feeds and deeper cuts. For finishing, a tool with a smaller nose radius and a sharper edge can produce a cleaner surface. The trade-off is that a finishing tool is less tolerant of deflection and setup error.
Match the insert to the material. Aluminum, stainless steel, and titanium each require different tool geometries and cutting speeds. A tool that works well on mild steel may chatter on stainless because the material is tougher and the cutting edge needs to stay sharper. Check the tooling data sheet for the material and the intended finish.
Replace worn tools before they reach the limit. A dull edge creates a higher cutting force and can push the tool into a vibration zone. If the surface finish has degraded without any change in parameters, inspect the insert. A small amount of wear can change the edge angle enough to cause chatter.
Prevention and routine checks
Prevention is simpler than troubleshooting. A short checklist before every run catches most problems. Check the tool holder for tightness. Check the overhang. Check the workholding. Check the cutting parameters. Check the tool wear. A two-minute inspection saves an hour of rework.
Keep a record of the parameters that worked. If a part cut cleanly at a certain speed and feed, use that as the baseline. If the finish changes, check the tool first, then the setup, then the parameters. This order avoids wasted time and prevents small issues from becoming large failures.
Train operators to recognize the sound and feel of a cut. A clean cut has a steady tone. A chattering cut has a buzzing or skipping sound. If the operator hears the change, stop the cycle and check the tool before the part is ruined. A small vibration early in the cut is easier to fix than a full run of ruined surfaces.
When to call for outside help
If the problem persists after checking tooling, setup, and parameters, the issue may be in the machine itself. Worn spindle bearings, a loose headstock, or a damaged way can cause vibration that no tool or program can fix. If multiple tools and multiple setups all chatter at the same spot, have the machine inspected. A machine that is not rigid will never produce a clean finish, no matter how good the tooling is.
Do not keep running a part that is failing the finish check. A bad surface can mask other defects and waste material. Stop, check, and fix. A single ruined part is cheap compared to a batch that fails inspection and has to be scrapped.
Frequently asked questions
Why does my CNC turning surface have ripple marks?
Ripple marks usually come from tool overhang, a loose holder, or unstable cutting parameters. Check the tool first, then the setup, then the speed and feed.
Can I fix chatter by slowing down the machine?
Sometimes. Lowering speed can reduce the force per cut and move the tool out of a deflection zone. If the finish is still poor, check the tool and setup before changing parameters again.
What is the best tool overhang for turning?
As short as the machine allows. A shorter overhang gives more rigidity and reduces the lever arm that causes vibration. Use the shortest holder or insert that reaches the work.
Do I need a steady rest for every long part?
Not always, but it helps for long bar stock and thin-walled parts. A steady rest supports the workpiece and keeps the tool from deflection into the unsupported section.
How do I know if the tool is worn?
Look for a change in surface finish, a change in tone, or a change in chip shape. A dull edge creates a higher cutting force and can push the tool into a vibration zone. Replace the insert before it reaches the limit.