Buyer's Guide: Sourcing CNC Parts for Prototyping
Selecting a supplier for low-volume prototype parts requires balancing speed, material choice, and post-processing. This guide outlines the specific cnc machining processes to evaluate, the supplier criteria to check, and a decision checklist for reducing risk in rapid prototyping projects.
- Match the process to the part geometry, not just the deadline.
- Verify supplier documentation requirements before releasing drawings.
- Use a decision checklist to compare quotes against technical capability.
Why Process Choice Drives Prototype Cost
Prototype parts often fail in the shop because the buyer picked the wrong CNC prototyping method. A simple bracket machined on a 3-axis mill may cost more than the same part made on a 5-axis machine if the design requires multiple setups.
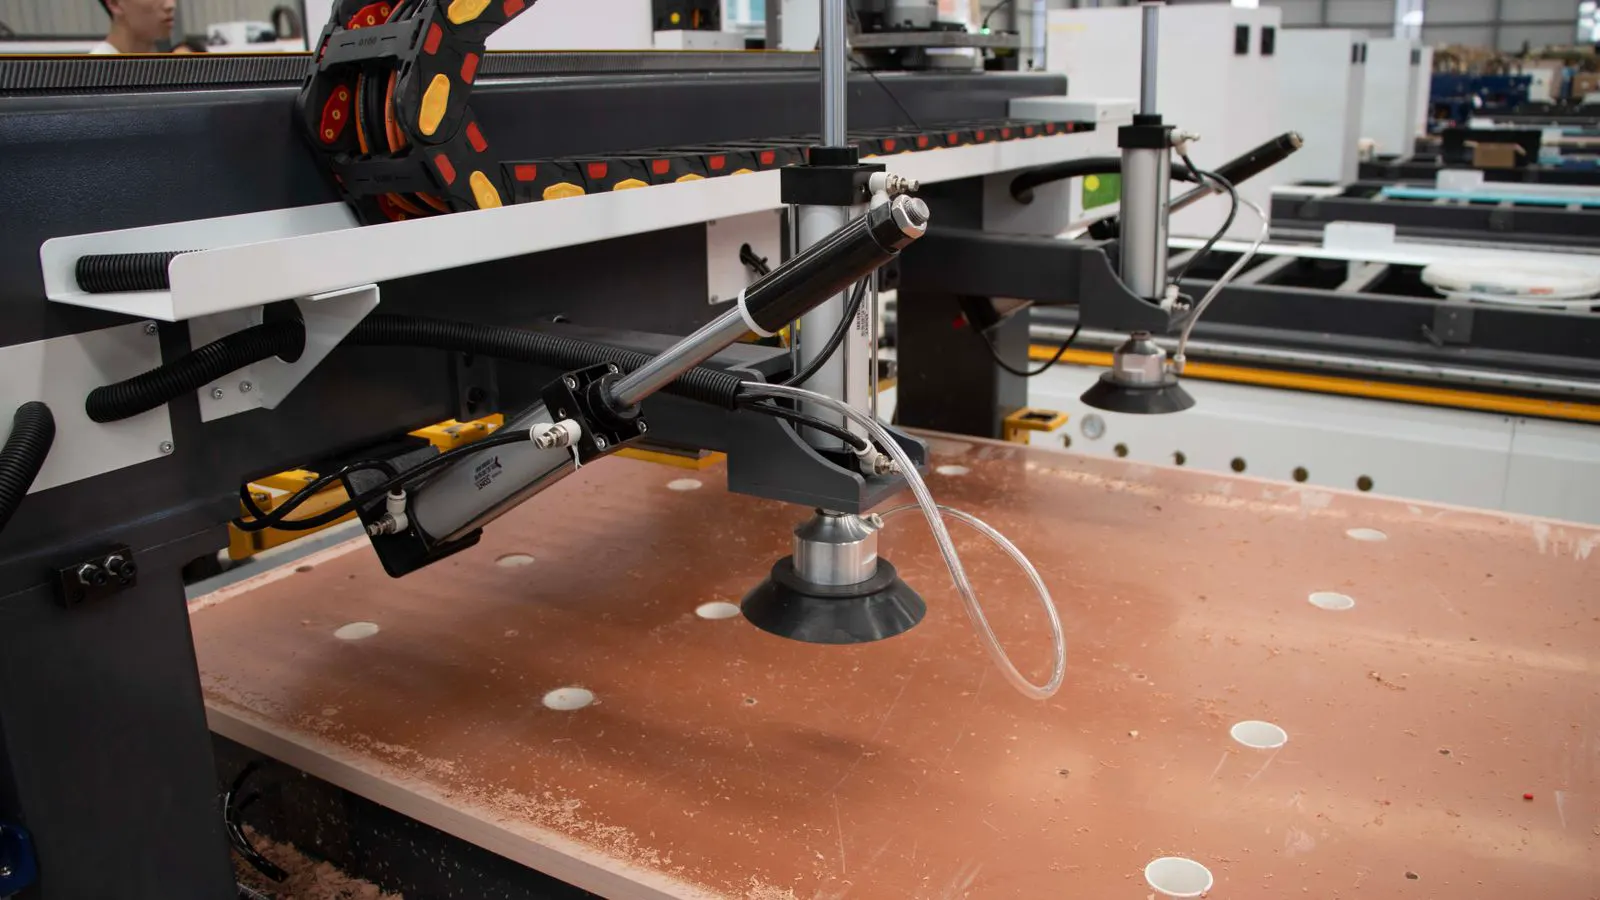
The CNC machining processes available to you usually fall into a few categories. Milling shapes parts from solid stock using rotating cutters. Turning handles round sections like shafts and bosses. Additive manufacturing builds parts layer by layer. Hybrid approaches combine these methods.
The choice affects three things: lead time, tolerance capability, and unit cost. For a one-off functional test, a 3-axis mill or a turning center may be the fastest path. For a complex aerospace bracket, a 5-axis mill or a hybrid process may be necessary to hold tight tolerances without a second setup.
Consider a specific example to understand the difference. A small housing with internal ribs and an angled mounting boss. On a 3-axis machine, the operator must clamp the part, machine the top surface, flip it, re-clamp, and machine the underside. Each flip adds setup time and introduces the risk of shifting the part. On a 5-axis machine, the part stays clamped in one position. The tool moves to reach the angled boss and the internal ribs in a single cycle. The part is often cheaper to make because the operator spends less time and the part spends less time in the fixture.
Another example is a shaft with multiple diameters and a keyway. Turning is the natural choice. A mill can make it, but it is inefficient. The shaft will show tool marks on the cylindrical surfaces, and the process takes longer. If the part also has a flat face, the supplier might use a mill-turn center. This machine handles both operations in one fixture.
Do not assume the most advanced machine is the best choice. If your part is a flat plate with through-holes, a 3-axis mill is sufficient. Paying for a 5-axis process adds cost without benefit. The right process is the one that matches the geometry, the material, and the quantity.
How to Evaluate Supplier Capability
Do not judge a supplier based on website graphics. Ask for the machine list. Look for the brand and model. Check the control software. Ask about the spindle speed and the tool changer capacity.
A good supplier will answer these questions without hesitation. They will tell you what their machines can do and what they cannot. They will point out design flaws before you release a drawing. They will ask about your material grade and heat treatment needs.
Bad suppliers will guess. They will promise a lead time they cannot keep. They will ignore your GD&T requirements until the part is late.
Use the criteria below to compare at least three suppliers.
| Criterion | What to look for | Why it matters |
|---|---|---|
| Machine Inventory | Specific models and axis count | Determines if your part can be made in one setup |
| Material Handling | In-house stock vs. external sourcing | Affects lead time and cost consistency |
| Quality Control | First article inspection reports | Proves they can hold your critical dimensions |
| Communication | Engineering contact availability | Reduces errors in drawing interpretation |
| Post-Processing | Deburring, anodizing, coating options | Saves you a second vendor for finishing |
When reviewing machine inventory, look beyond axis count. A 5-axis machine with a small spindle and a limited tool changer may struggle with a part that requires deep pockets or large end mills. Ask about the maximum part size. Ask about the maximum spindle power. If your part is made of hardened tool steel, you need a machine with high rigidity and strong cooling.
Material handling is a hidden cost driver. If a supplier stocks common materials like 6061 aluminum or 303 stainless steel, they can start cutting immediately. If they must order a special alloy or a specific heat treatment, the lead time jumps. Ask where they source their stock. Ask if they have a safety stock for common grades.
Quality control is not just about having a CMM. It is about what they do with the data. Ask if they inspect every part or just the first one. For prototypes, a full first article inspection is standard. For small batches, they may inspect 100 percent of critical dimensions. If they only do visual checks, you are taking a risk.
Communication is the most underappreciated criterion. A supplier with a responsive engineering contact will catch a missing dimension before it becomes a problem. A supplier with a sales-only contact will quote the part and wait for you to call with a problem. Ask who you will talk to when the drawing is in hand. Ask if they have a dedicated engineering support line.
Post-processing options save time and money. If the supplier can anodize, paint, or plate in-house, you avoid shipping the part to a second vendor. You also keep the part under one roof for quality control. If the supplier outsources finishing, ask who the second vendor is. Ask how long the turnaround is.
Understanding Tolerances and Finish
Prototype parts are not always held to production tolerances. But a bad tolerance call here creates a part that will not fit the assembly.
Ask your supplier about their standard tolerances. If you do not specify, they will apply their default. For many general CNC prototyping jobs, the default might be plus or minus 0.1 mm. For a bearing bore, you might need plus or minus 0.01 mm.
Surface finish is another factor. A rough machined surface looks different from a polished one. If the part is for a customer demo, you might need a fine finish. If it is for internal testing, a standard finish is usually enough.
Do not specify a finish you do not need. A mirror finish costs more and takes longer. Specify the minimum finish required for the function.
Tolerances are not just about size. They are about position, orientation, and flatness. A hole that is the right diameter but off-center by 0.2 mm may not fit a shaft. A face that is flat but warped by 0.1 mm may not seal against a gasket. When you draw your part, identify the critical dimensions. Mark them clearly. If you do not mark them, the supplier will use their default, which may be too loose for your application.
Use standard GD&T symbols when possible. They reduce ambiguity. A “parallelism” call is clearer than a “flatness” call in some cases. A “perpendicularity” call tells the supplier exactly how the feature relates to the datum. If you are not familiar with GD&T, ask your supplier to review your drawing. They will point out where the tolerances are too tight or too loose.
Surface finish is often specified in microinches or microns. For a prototype, a standard finish of 1.25 to 2.5 microns is usually sufficient. For a cosmetic part or a part that will be seen by customers, you might need 0.8 microns or better. For a functional part that will be coated, the finish matters less. The coating will cover the tool marks.
Do not mix up tolerance and finish. A tight tolerance does not require a smooth finish. A smooth finish does not require a tight tolerance. A bearing bore needs a tight tolerance to ensure proper fit. It does not need a mirror finish. A decorative cover needs a good finish, but the dimensions can be loose as long as the part looks right.
Managing Materials and Lead Time
Material selection changes the entire CNC machining process. Aluminum is easy to cut. It is light and cheap. Stainless steel is tougher. It requires slower feed rates and stronger tools.
For rapid prototyping, pre-machined bar stock or plate is common. The supplier cuts the raw material to size. This saves time. If you need a specific grade, like 6061-T6 aluminum, state it on the drawing. Do not assume the supplier will pick the best grade.
Lead time depends on two things. How long does the machine take to cut the part, and how long does the queue take? A simple part on a busy machine may take weeks. A complex part on an idle machine may take days.
Ask for a realistic date. If the supplier gives you a date that seems too fast, ask how. Do they have the material on hand? Do they have an open slot on the machine.
Material choice also affects the machine tool. Aluminum chips are soft and can clog the chip conveyor. Stainless steel chips are springy and can stick to the tool. Inconel is even harder. It requires high-end tools and long cutting times. If you choose a difficult material, expect a higher cost and a longer lead time.
For prototypes, consider using a material that is easy to machine. If your production part is made of titanium, use aluminum or steel for the prototype. This allows you to test the design and the assembly without the cost and time of hard-to-machine metals. Once the design is proven, switch to the production material.
Lead time is often underestimated. The cutting time is just one part of the equation. You also have to wait for the material. You have to wait for the machine schedule. You have to wait for inspection. You have to wait for post-processing. A part that takes 2 hours to cut may take 2 weeks to deliver if the machine is booked.
When asking for a quote, ask for a lead time breakdown. Ask how long the material takes to arrive. Ask how long the machine time is. Ask how long the inspection takes. Ask how long the shipping takes. This gives you a clear picture of the total time.
If your project has a hard deadline, tell the supplier. They may have a faster option. They may have a machine that is free. They may have the material in stock. If they do not, do not take their word for it. Ask for evidence. Ask for the machine schedule. Ask for the material order number.
Post-Processing and Inspection
The cut part is not the final part. It needs deburring. It may need a surface treatment. It needs inspection.
Deburring removes sharp edges from the cut. This is usually included in the base price. But special deburring, like hand deburring or laser deburring, costs more.
Surface treatments include anodizing, painting, or plating. These change the part’s appearance and corrosion resistance. For a prototype, you might skip plating to save time. For a customer sample, you might add it to match the production spec.
Inspection is where most errors hide. Ask for a first article inspection report. This document lists every critical dimension and shows the measured value. If a dimension is out of spec, the report will show it.
Do not accept a part without the report if the dimensions are critical. The part may look perfect, but a hidden tolerance violation will cause a fit issue later.
Deburring is not just about aesthetics. Sharp edges are a safety hazard. They can cut the operator or the user. They can also cause stress concentrations that lead to failure. A well-deburred part lasts longer. A poorly deburred part may fail in the field.
Surface treatments serve multiple purposes. Anodizing increases the hardness of the surface. It also adds color. Painting provides a barrier against corrosion. Plating, like zinc or nickel, adds a layer of metal that protects the part. For a prototype, you may skip these treatments to save time. But if the part will be used in a corrosive environment, you may need to add them.
Inspection is a critical step. A first article inspection report is a document that proves the part meets the drawing. It lists every critical dimension. It shows the measured value. It shows the tolerance. It shows the result: pass or fail.
If a dimension is out of spec, the report will show it. This is valuable. It tells you what needs to be fixed. It also protects you. If the part fails later, you have proof that the supplier checked the dimensions.
Do not rely on visual inspection. A part can look perfect and still be out of tolerance. A hole can be the right diameter but the wrong depth. A face can be flat but the wrong thickness. Only measurement tools like a CMM, a micrometer, or a caliper can verify the dimensions.
Ask the supplier what tools they use for inspection. Ask if they use a CMM for complex parts. Ask if they use optical comparison for small features. Ask if they use a bore gauge for internal diameters. The more tools they have, the more accurately they can measure.
If the part is a prototype, you may not need 100 percent inspection. You may only need the first part inspected. But if the part is a batch of 10 or 20, you may need each part inspected. Ask the supplier what their standard practice is for your quantity.
Decision Checklist for Sourcing
Use this checklist before you send your drawings to a supplier.
- Check the drawings. Are all dimensions and tolerances defined?
- Select the material. Is the grade specified?
- Identify the process. Does the part need milling, turning, or both?
- Define the finish. What is the minimum surface requirement?
- Set the quantity. How many parts are you ordering?
- Request a quote. Ask for a firm lead time.
- Review the FAI. Confirm the inspection report is included.
This checklist takes five minutes. It prevents the most common sourcing errors. It forces you to think like the supplier does. It clarifies your requirements before the money is spent.
When checking the drawings, look for missing information. Are there any dimensions that are implied but not drawn? Are there any tolerances that are not specified? Are there any features that are not defined? If you are unsure, ask the supplier. They will catch these issues. They will not guess. They will ask you to clarify.
When selecting the material, think about the function. Is the part structural? Is it decorative? Is it for a high-temperature environment? Choose a material that fits the function. Do not choose a material just because it is cheap. A cheap material that fails will cost more than a better material that works.
When identifying the process, think about the geometry. Is the part mostly flat? Is it mostly round? Is it complex? Choose a process that matches the geometry. Do not force a complex part onto a simple machine. Do not use a simple machine for a complex part.
When defining the finish, think about the appearance. Is the part for a customer? Is it for internal testing? Choose a finish that matches the purpose. Do not pay for a finish that no one will see.
When setting the quantity, think about the cost. A single part is expensive. Ten parts are cheaper per unit. Fifty parts are cheaper still. The quantity affects the cost. It also affects the lead time. A single part may take longer to make than ten parts, because the setup time is spread over fewer parts.
When requesting a quote, ask for a firm lead time. Do not accept a range. Ask for a date. If the date is not firm, ask why. Ask if they have the material. Ask if they have the machine. Ask if they have the staff.
When reviewing the FAI, check the report. Does it list all the critical dimensions? Does it show the measured values? Does it show the pass or fail status? If the report is missing or incomplete, ask for it. Do not accept a part without the report.
Common Mistakes in Low-Volume Builds
Buyers often make the same mistakes with CNC prototyping.
The first mistake is vague drawings. They omit critical features. They leave tolerances blank. They do not define the material.
The second mistake is ignoring the process. They send a complex 3D model to a supplier with only 3-axis capability. The part takes twice as long to make.
The third mistake is skipping the FAI. They receive the parts and install them. The next day, the assembly fails. They do not have the inspection data to prove the error.
The fourth mistake is choosing the cheapest quote. The cheapest supplier often has the longest lead time. They may not have the material on hand. They may not have the machine capability.
Avoid these mistakes by preparing your data well and asking the right questions.
The first mistake is vague drawings. This is the most common error. A drawing that is missing a dimension, a tolerance, or a material grade is a recipe for delay. The supplier will quote the part based on assumptions. They will make the part based on assumptions. When the part arrives, it may not fit. You have to send it back for rework. You lose time. You lose money.
The second mistake is ignoring the process. This happens when the buyer does not know the capabilities of the supplier. They send a complex model to a basic shop. The shop has to make multiple setups. They have to flip the part. They have to re-clamp it. The process is slow. The cost is higher. The lead time is longer. If you know the process, you can choose a better supplier. You can design the part to fit the process. You can save time and money.
The third mistake is skipping the FAI. This is a dangerous error. A prototype part is not just a part. It is a test. It is a proof. If the part fails, you need to know why. You need the inspection data. You need to know which dimension was out of spec. Without the FAI, you are guessing. You are wasting money. You are delaying the project.
The fourth mistake is choosing the cheapest quote. This is a trap. The cheapest supplier is often the worst supplier. They have the longest lead time. They have the least capability. They have the worst communication. They may not have the material. They may not have the machine. They may not have the staff. When the part is late, you are stuck. You have to find a new supplier. You have to re-quote the part. You have to re-send the drawings. You lose time. You lose money.
Avoid these mistakes by preparing your data well. Do your homework. Check the drawings. Select the material. Identify the process. Define the finish. Set the quantity. Request a quote. Review the FAI. Ask the right questions. These steps will save you time and money. They will ensure that your prototype part is made correctly. They will ensure that your project stays on track.
Frequently asked questions
Can I use the same supplier for production and prototyping?
Yes, many suppliers handle both. They may use different machines for each. A prototype might go on a high-speed mill, while production parts go on a larger machine. Ask which setup they will use.
How many sets of drawings should I send?
Send the latest revision only. Label it clearly. If you have multiple versions, delete the old ones from the file. This prevents the supplier from cutting the wrong version.
Is additive manufacturing better for prototypes?
Not always. Additive is great for complex geometry. But it may not hold the tolerances you need. For a simple bracket, cnc prototyping is faster and more accurate.
What if my part needs multiple operations?
Ask the supplier if they can do it in one setup. If not, ask for a process plan. This shows you exactly how many times the part will be handled.
How do I handle changes during production?
Freeze the drawings once the job starts. If you need a change, request a formal revision. The supplier will quote the extra work and the new lead time. This prevents disputes later.